E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Tan Xinyue — After-Sales Technical Coordinator / High-Performance SMC Stator Core for Efficient Motor Applications
High-Performance SMC Stator Core for Efficient Motor Applications
 2026.11.09
 Tan Xinyue — After-Sales Technical Coordinator
Content
- 1 1. Product Overview
- 2 2. Why the Stator Core Matters in Motor Design
- 3 3. Material Characteristics of SOMALOY 700HR-3P
- 4 4. Principal Advantages Compared with Conventional Core Solutions
- 5 5. Powder Metallurgy Manufacturing Process
- 6 6. Influence of Particle Size and Coating on Performance
- 7 7. Technical Specification Summary
- 8 8. Application Areas
- 9 9. Manufacturing Strengths of Jiande Welfine Technology Co., Ltd.
- 10 10. Quality and Reliability Considerations
- 11 11. Packaging and Delivery
- 12 12. Customization and Product Development Process
- 13 13. Selection Guidance for Buyers and Motor Designers
- 14 14. Frequently Asked Questions
- 14.1 14.1 What is an SMC stator core?
- 14.2 14.2 How does an SMC stator core differ from a laminated silicon steel core?
- 14.3 14.3 Why is SOMALOY 700HR-3P suitable for inverter motors?
- 14.4 14.4 Can the stator core be customized?
- 14.5 14.5 What information is required for a quotation?
- 14.6 14.6 How is the insulation coating protected during compaction?
- 14.7 14.7 Can SMC stator cores operate at high temperature?
- 14.8 14.8 What applications are suitable for this product?
- 14.9 14.9 Does the company support small trial orders?
- 14.10 14.10 How should finished stator cores be stored?
- 15 15. Conclusion
- 16 References
- 17 Product: SMC Stator Core (SOMALOY 700HR-3P)
Modern motor manufacturers are under continuous pressure to improve energy efficiency, reduce operating noise, control weight, and maintain reliable performance over long service lives. These requirements are especially important in inverter air conditioners, commercial HVAC equipment, fresh-air systems, air purifiers, and other appliances that operate under variable speed, high-frequency, or high-load conditions. The stator core is one of the most important components in meeting these objectives because it directly influences magnetic flux distribution, core loss, motor efficiency, thermal behavior, and assembly accuracy.
The SMC stator core made from SOMALOY 700HR-3P is a high-performance soft magnetic composite component developed for demanding motor applications. Produced through powder metallurgy compaction, sintering, and precision post-processing, the component combines three-dimensional magnetic circuit capability with low eddy current loss, high permeability, controlled dimensional accuracy, and a lightweight structure. Its ring-shaped toothed design is suitable for axial-flux and high-efficiency motor architectures, including household inverter air conditioner motors and commercial fan motors.
Jiande Welfine Technology Co., Ltd. manufactures this type of precision magnetic component using a controlled powder metallurgy process supported by modern pressing, sintering, forming, inspection, and machining capabilities. With more than two decades of experience in powder metallurgy and precision components, the company provides OEM and ODM solutions based on customer drawings, samples, performance targets, and application requirements.
This article explains the material characteristics, manufacturing process, technical advantages, application value, quality control methods, customization capabilities, and selection considerations associated with the SMC stator core.
1. Product Overview
An SMC stator core is a magnetic circuit component formed from electrically insulated ferromagnetic powder particles. Unlike a conventional laminated silicon steel core, which is generally assembled from stacked two-dimensional sheets, an SMC component is compacted into a three-dimensional geometry. This makes it possible to form integrated teeth, grooves, curved surfaces, and other complex magnetic structures in a single pressing operation.
The featured component uses SOMALOY 700HR-3P, a high-performance soft magnetic composite grade designed to provide a balance of magnetic performance, electrical resistivity, mechanical strength, and thermal stability. The stator has a ring-shaped toothed configuration and is designed for motor assemblies requiring accurate alignment between the magnetic core, windings, housing, and rotating components.
The current model is identified as L1C10000557A-001A. Its nominal outer diameter is 100.0 mm, the nominal inner diameter is 65.0 mm, and its thickness is 10.0 mm. The part has 18 teeth and is manufactured with controlled tooth profile accuracy, flatness, parallelism, and overall dimensional tolerances.
Although the supplied configuration is associated with Midea air conditioner motor applications, the underlying design and manufacturing technology can also be adapted to other motor platforms. Customers may provide drawings, samples, three-dimensional data, or performance specifications for engineering evaluation and OEM or ODM production.
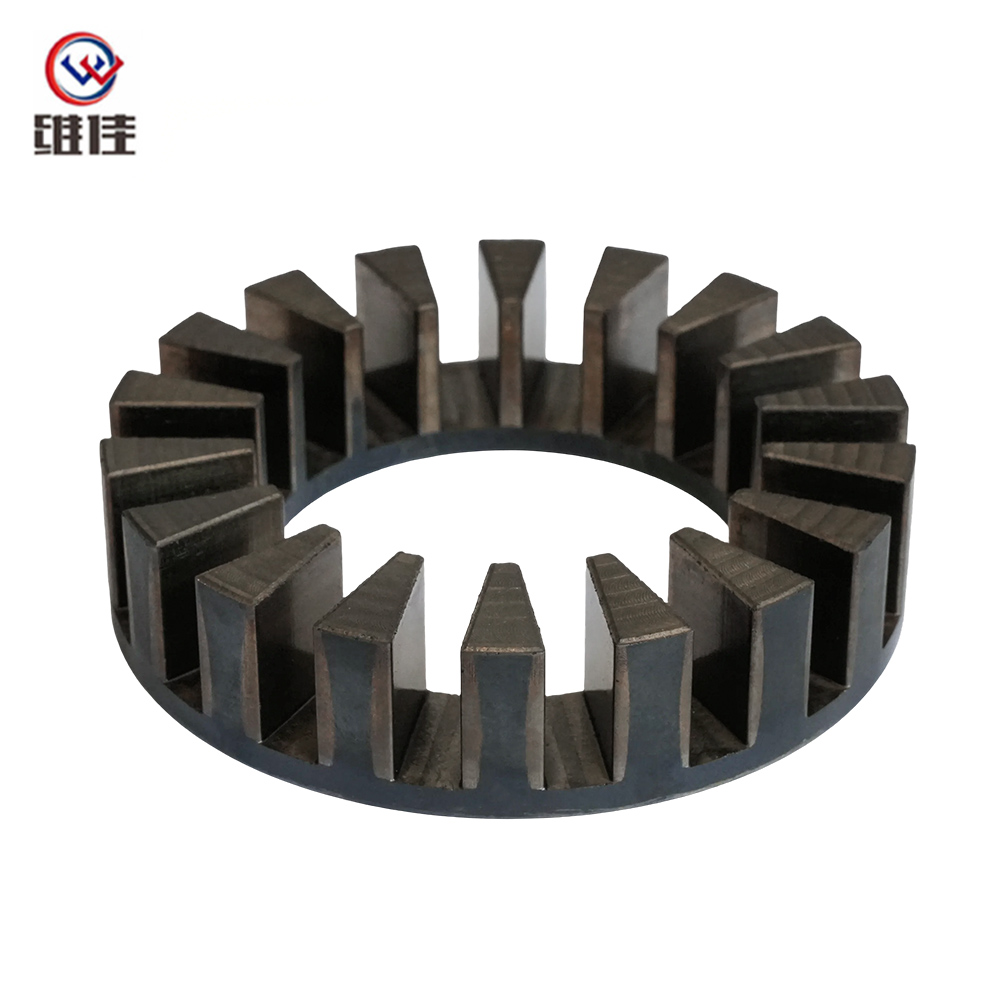
SMC Stator Core (SOMALOY 700HR-3P)
2. Why the Stator Core Matters in Motor Design
The stator core guides magnetic flux and supports the motor windings. Its geometry determines how efficiently electromagnetic energy is transferred between the stationary and rotating parts of the motor. Small variations in tooth shape, air-gap alignment, concentricity, or surface flatness can affect torque ripple, acoustic noise, vibration, temperature rise, and energy consumption.
In conventional motors, the stator core is often manufactured from laminated electrical steel. Laminations are effective for many applications, but they can limit the designer’s ability to create complex three-dimensional magnetic paths. They also require additional operations such as stamping, deburring, stacking, bonding, riveting, or welding. Each operation introduces potential variation and increases the number of interfaces in the finished assembly.
Soft magnetic composites offer a different design approach. Individual iron-based particles are surrounded by an electrically insulating coating. During compaction, the particles are formed into the required shape while retaining electrical isolation between neighboring particles. The resulting component can carry magnetic flux in multiple directions and can be manufactured as a near-net-shape part with integrated teeth and other geometric features.
This three-dimensional capability is valuable in axial-flux motors and other high-efficiency motor structures where magnetic flux does not remain entirely within a single planar direction. It also allows engineers to explore more compact magnetic circuits, improved winding utilization, and reduced component count.
3. Material Characteristics of SOMALOY 700HR-3P
SOMALOY 700HR-3P is used in this stator core because it provides a combination of magnetic and mechanical properties suitable for high-efficiency motor applications. The insulated particle structure helps increase electrical resistivity compared with conventional bulk iron, thereby limiting circulating eddy currents within the material.
The material is designed for conditions in which the magnetic field changes frequently. This is particularly relevant to inverter-driven motors because variable-frequency operation can expose the core to a broad range of electrical frequencies. At higher frequencies, eddy current losses can become a significant source of heat and efficiency reduction if the magnetic core is not properly designed.
The target material and physical properties for the component include a density of at least 6.5 g/cm³, electrical resistivity of at least 80 μΩ·cm, hardness of at least 180 HV, and bending strength of at least 400 MPa. The stated coefficient of thermal expansion is 12 × 10⁻⁶/℃ over the range from 20℃ to 100℃.
These values provide a useful balance. Higher density generally supports improved magnetic flux carrying capability, while adequate electrical resistivity helps reduce eddy current loss. Mechanical strength is essential because the stator must withstand handling, winding operations, assembly forces, vibration, and long-term thermal cycling.
3.1 Magnetic Performance
The specified magnetic performance includes a saturation magnetic induction of at least 1.5 T, an initial permeability of at least 300 μ₀, and a maximum permeability of at least 1000 μ₀. The coercivity target is no greater than 20 A/m. These characteristics allow the stator core to respond effectively to changing magnetic fields while limiting the magnetic field strength required to establish flux.
The stated core loss is no greater than 1.5 W/kg at 1.0 T and 50 Hz, and no greater than 12 W/kg at 1.0 T and 400 Hz. Actual results depend on test method, specimen geometry, compaction density, coating condition, processing history, and operating temperature. Therefore, application-specific validation should be performed using agreed testing standards and representative production samples.
3.2 Thermal and Environmental Performance
The operating temperature range is specified as -40℃ to 180℃. This range is suitable for many household appliance and HVAC motor environments, where the core may experience repeated heating and cooling cycles. The stated dielectric withstand voltage is at least 500 VAC for one minute.
The component is also specified to show no significant rust after a 48-hour neutral salt spray test and no cracking after 10 thermal shock cycles between 150℃ and room temperature. These requirements support reliable operation in environments involving humidity, temperature variation, and extended service periods.
4. Principal Advantages Compared with Conventional Core Solutions
4.1 Three-Dimensional Magnetic Circuit Design
The most important advantage of an SMC stator core is its ability to support three-dimensional magnetic flux paths. In a laminated core, the material and assembly direction are strongly associated with the plane of the electrical steel sheets. An SMC component is compacted as a three-dimensional body, allowing magnetic circuit designers greater freedom when developing axial-flux, transverse-flux, or other unconventional motor structures.
This design flexibility can help reduce magnetic leakage, improve the use of available motor space, and simplify the integration of teeth or other features. It can also support more compact motor designs where traditional lamination arrangements would require multiple subassemblies.
4.2 Reduced Eddy Current Loss at Elevated Frequency
Every iron particle in an SMC material is separated from neighboring particles by an insulating coating. This structure interrupts large circulating electrical paths and helps reduce eddy current formation. The benefit becomes increasingly important as switching frequency, motor speed, or magnetic field variation increases.
Reduced core loss can contribute to lower temperature rise, improved motor efficiency, increased continuous operating capability, and reduced cooling requirements. For inverter air conditioner motors, these benefits may support more efficient variable-speed operation across cooling and heating cycles.
4.3 Integrated Near-Net-Shape Forming
Complex teeth and ring-shaped geometries can be formed during a single compaction operation. Compared with processes that require stamping and stacking many individual laminations, powder metallurgy can reduce the number of assembly interfaces and simplify the production route.
Near-net-shape forming also reduces the amount of material removed during machining. This can improve material utilization and create opportunities to manufacture integrated features that would be difficult or costly to produce using sheet-metal methods.
4.4 Lightweight Motor Construction
The SMC stator core can support a lightweight motor design compared with certain traditional core arrangements. Lower component weight may simplify handling, reduce system mass, and improve dynamic response. In household appliances, reducing motor weight can also support compact product architecture and easier integration into the overall air conditioner or appliance assembly.
4.5 Lower Noise Potential
A uniform magnetic circuit and accurate tooth geometry help control variations in magnetic force. Together with the low magnetostriction characteristics associated with suitable SMC materials, this may help reduce vibration and operating noise. Noise performance is particularly important in residential air conditioners, fresh-air systems, and air purification equipment, where the motor often operates close to occupants.
4.6 Reduced Core Assembly Complexity
A molded stator core can reduce the requirement for multiple stacked components, alignment steps, and joining operations. Fewer interfaces can improve consistency and reduce possible sources of dimensional variation. The final result depends on the design, material formulation, tooling, and process controls, but the production concept offers clear opportunities for simplifying certain motor assemblies.
5. Powder Metallurgy Manufacturing Process
5.1 Powder Selection and Preparation
The manufacturing process begins with the selection of suitable soft magnetic powder. Important considerations include chemical composition, particle morphology, particle size distribution, apparent density, flowability, compressibility, and coating compatibility.
Particle size must be controlled carefully. Very fine particles can provide a large surface area for insulation and may support good high-frequency performance, but they can also increase inter-particle friction and reduce compacting efficiency. Very coarse particles may flow well and compact easily, but excessive coarseness can increase porosity and reduce magnetic performance.
An optimized particle size distribution combines different particle fractions to improve packing efficiency. Fine particles can fill spaces between larger particles, while coarser particles may support material flow and compaction. The exact formulation must be established through laboratory testing, trial compaction, density measurement, and magnetic evaluation.
5.2 Insulation Coating Control
The insulation coating is one of the most critical features of an SMC material. It must electrically isolate the iron particles while maintaining sufficient magnetic contact and mechanical integrity. A coating that is too thin or discontinuous may allow excessive inter-particle eddy currents. A coating that is too thick may reduce magnetic contact and create a magnetic dilution effect.
Coating adhesion is equally important. During filling, compaction, ejection, heat treatment, and handling, the coating must resist damage. Cracked or detached coating can increase core loss and may create local variations in electrical resistivity. The coating system must therefore be selected and processed according to the material grade, compaction pressure, heat-treatment profile, and final operating conditions.
5.3 Powder Mixing and Lubrication
Controlled mixing ensures that the powder, coating, lubricant, and any approved additives are distributed uniformly. Lubrication reduces friction between powder particles and between the compact and the tooling. However, excessive lubricant can lower green strength, influence density distribution, and affect the final magnetic properties.
Mixing time, temperature, humidity, and storage conditions may influence powder flow and coating stability. A controlled material-handling system helps maintain consistent batch behavior and reduces variation during high-volume production.
5.4 Die Filling and Compaction
The prepared powder is loaded into a precision die designed for the ring-shaped toothed stator geometry. Accurate filling is necessary because uneven powder distribution can create density gradients. Density variation may influence local permeability, mechanical strength, dimensional shrinkage, and magnetic loss.
Compaction pressure, pressing speed, dwell time, tooling condition, and ejection speed must be controlled. The die must produce the specified outer diameter, inner diameter, tooth profile, and thickness while minimizing damage to the insulated powder particles.
Forming the complete toothed structure in one pressing operation can improve tooth-to-ring alignment and reduce the need for extensive post-machining. The tooling design must nevertheless account for powder flow, density distribution, ejection forces, dimensional springback, and potential cracking at sharp transitions.
5.5 Heat Treatment and Sintering
After compaction, the component undergoes a controlled thermal process. The precise schedule depends on the SMC material system and the required balance of strength, dimensional stability, insulation retention, and magnetic performance. The process must remove or stabilize process additives without damaging the particle insulation layer.
Atmosphere control, temperature uniformity, heating rate, cooling rate, and furnace loading are important process variables. Excessive temperature or an unsuitable atmosphere may degrade the coating or alter the magnetic properties. Insufficient treatment may leave residual materials or reduce mechanical integrity.
Jiande Welfine Technology Co., Ltd. operates high-temperature sintering furnaces and applies controlled thermal processing to powder metallurgy components. Production conditions are monitored to support repeatable results between batches.
5.6 Precision Post-Processing
Although the stator is formed close to its final shape, selected surfaces or features may require post-processing. Precision machining, sizing, deburring, surface correction, or dimensional calibration can be applied where necessary. The objective is to achieve the required assembly accuracy without removing excessive material or damaging the magnetic structure.
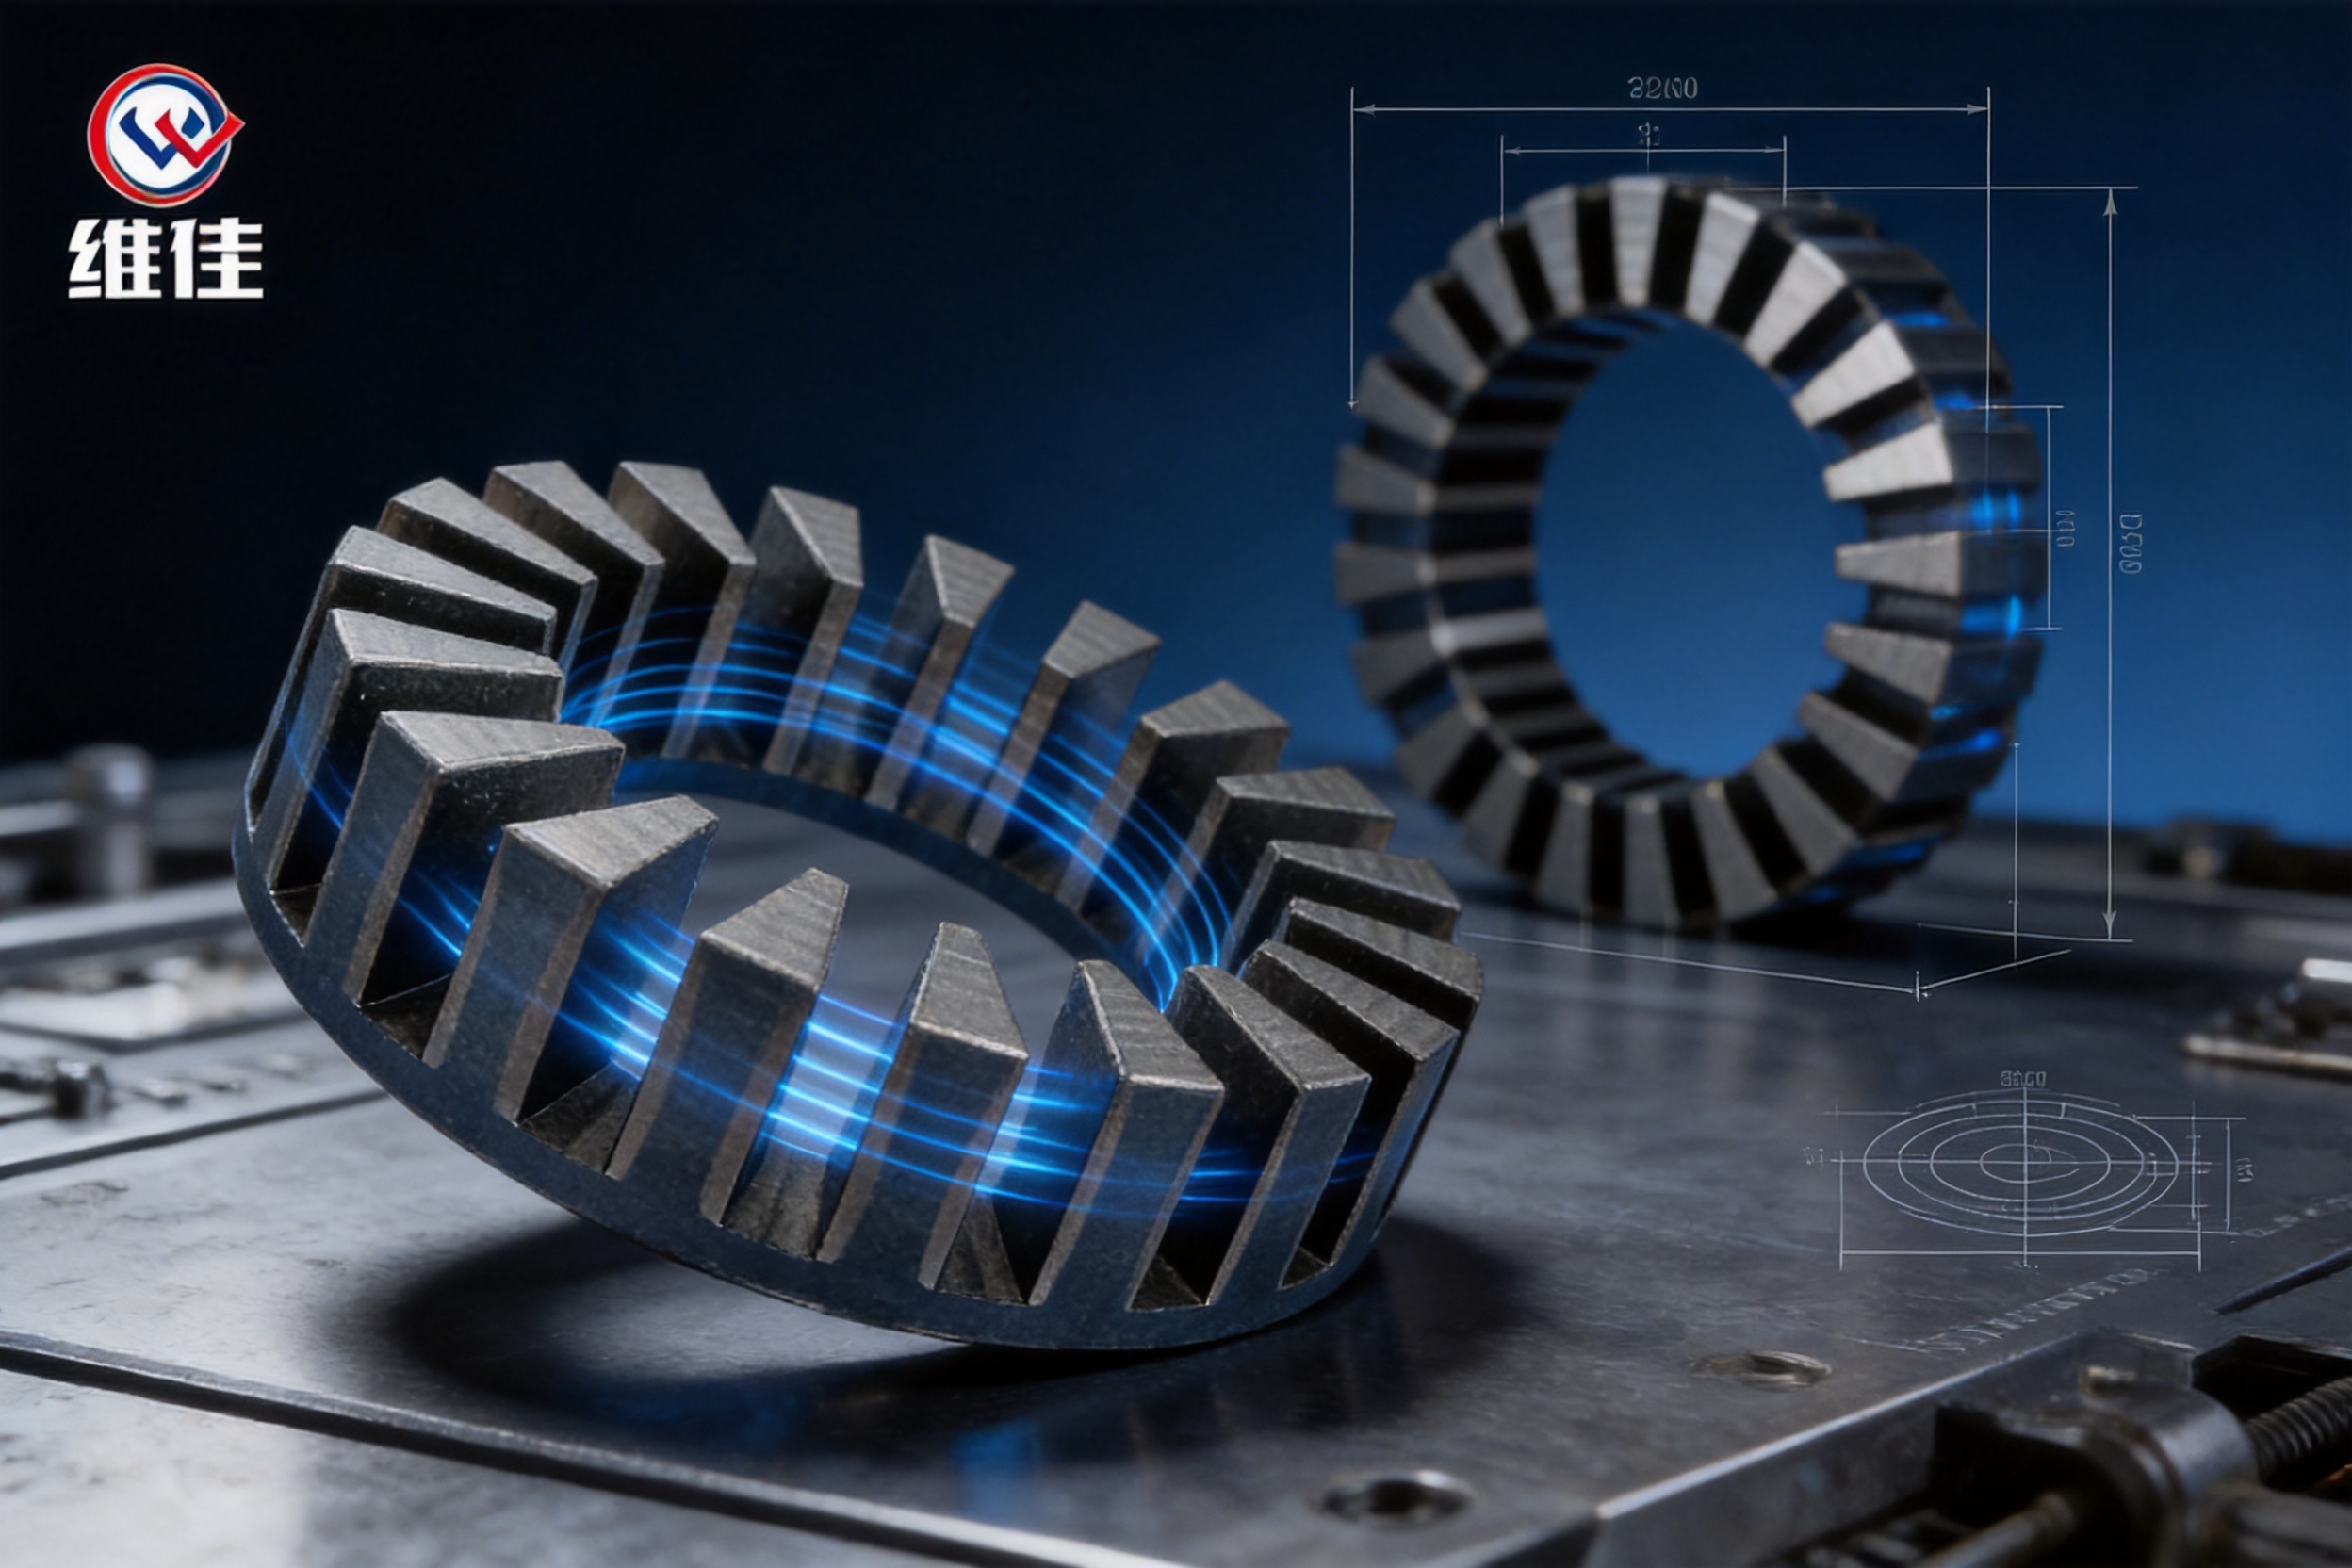
For the stated model, the target dimensional requirements include an outer diameter of Φ100.0 ±0.1 mm, an inner diameter of Φ65.0 ±0.1 mm, and a thickness of 10.0 ±0.05 mm. Tooth profile tolerance is controlled to ±0.03 mm, flatness to no more than 0.05 mm, and parallelism to no more than 0.03 mm.
5.7 Inspection and Release
Inspection may include dimensional measurement, density testing, hardness testing, mechanical strength evaluation, electrical resistivity measurement, magnetic testing, surface examination, and functional assembly checks. The appropriate inspection plan depends on the customer drawing, purchase specification, application risk, and production volume.
Traceability from raw powder batch through pressing, thermal processing, post-processing, inspection, packaging, and delivery helps identify process trends and supports corrective action. This is especially important for motor components supplied to appliance and automotive-related customers.
6. Influence of Particle Size and Coating on Performance
Particle size distribution and insulation coating quality interact with nearly every important property of an SMC stator core. They influence permeability, core loss, density, green strength, final mechanical strength, dimensional stability, and process productivity.
6.1 Particle Size and Magnetic Permeability
Smaller particles provide a greater number of particle boundaries and can help reduce the scale of eddy current paths. They may also support a more uniform coating distribution. However, fine powders can have higher surface friction, lower flowability, and greater resistance to compaction.
Coarse particles often have better flow characteristics, but excessive coarse material can result in larger pores or less uniform packing. Porosity reduces the effective magnetic cross-sectional area and may lower permeability. An optimized mixture can improve packing density and provide a more balanced combination of flowability, magnetic response, and strength.
6.2 Coating Thickness and Core Loss
A continuous coating is necessary to electrically separate adjacent particles. If the coating is damaged during compaction or thermal processing, local electrical paths may form and increase eddy current loss. If the coating is too thick, it occupies a greater proportion of the component volume and reduces the amount of magnetically active material.
The best result is not necessarily achieved by using the thinnest possible coating. The coating must be thick enough to provide reliable insulation under the intended frequency and temperature conditions while remaining thin and uniform enough to preserve magnetic performance.
6.3 Particle Size and Mechanical Strength
Mechanical strength depends on particle contact, density, bonding, coating condition, compaction pressure, and thermal treatment. An optimized particle gradation can increase the contact area between particles and reduce internal voids. This supports improved green strength and better final structural integrity.
Very fine particles may provide high green strength under some conditions, but they can also increase friction and complicate filling. Coarse particles may flow easily but leave more porosity. The formulation must therefore be matched to the die design and the required component geometry.
6.4 Coating and Mechanical Integrity
The coating must survive compaction without excessive cracking. A brittle coating may provide good electrical resistance but reduce mechanical strength if it fractures at particle contacts. A coating with better adhesion and appropriate flexibility can support both electrical insulation and structural reliability.
Organic or polymer-containing systems may improve handling and green strength, while inorganic or phosphate-based systems can provide useful thermal and electrical characteristics. The final selection depends on the required operating temperature, magnetic performance, mechanical strength, and production process.
7. Technical Specification Summary
| Category | Parameter | Specification |
|---|---|---|
| Material | Material grade | SOMALOY 700HR-3P |
| Physical | Density | ≥6.5 g/cm³ |
| Physical | Electrical resistivity | ≥80 μΩ·cm |
| Physical | Hardness | ≥180 HV |
| Physical | Bending strength | ≥400 MPa |
| Thermal | Coefficient of thermal expansion | 12 × 10⁻⁶/℃ from 20℃ to 100℃ |
| Magnetic | Saturation magnetic induction | ≥1.5 T |
| Magnetic | Initial permeability | ≥300 μ₀ |
| Magnetic | Maximum permeability | ≥1000 μ₀ |
| Magnetic | Coercivity | ≤20 A/m |
| Magnetic | Core loss at 1.0 T/50 Hz | ≤1.5 W/kg |
| Magnetic | Core loss at 1.0 T/400 Hz | ≤12 W/kg |
| Environmental | Operating temperature | -40℃ to 180℃ |
| Electrical | Dielectric withstand voltage | ≥500 VAC for 1 minute |
| Reliability | Neutral salt spray | No significant rust after 48 hours |
| Reliability | Thermal shock | No cracking after 10 cycles from 150℃ to room temperature |
| Dimensions | Outer diameter | Φ100.0 ±0.1 mm |
| Dimensions | Inner diameter | Φ65.0 ±0.1 mm |
| Dimensions | Thickness | 10.0 ±0.05 mm |
| Geometry | Number of teeth | 18 |
| Geometry | Tooth profile tolerance | ±0.03 mm |
| Geometry | Flatness | ≤0.05 mm |
| Geometry | Parallelism | ≤0.03 mm |
The specifications in this table are reference targets for the stated product configuration. Final acceptance criteria should be confirmed through the approved engineering drawing, technical agreement, inspection standard, and application-specific validation plan.
8. Application Areas
8.1 Household Inverter Air Conditioner Motors
Inverter air conditioners continuously adjust compressor and fan speed to match cooling or heating demand. Their motors must operate efficiently over a wide frequency range rather than at a single fixed operating point. The SMC stator core is suitable for indoor and outdoor drive motors where low loss, low noise, compact dimensions, and reliable thermal performance are required.
The component is particularly suitable for household air conditioner models of approximately 1.5 horsepower and above, subject to motor design verification. Its low-loss magnetic structure can help support rapid cooling and heating, reduced energy consumption, and compliance with demanding energy-efficiency objectives.
8.2 Commercial HVAC Fan Motors
Commercial multi-split systems, ducted air conditioners, and central HVAC equipment often operate for long periods. Their fan motors must provide stable output while resisting thermal stress, vibration, and environmental exposure.
An accurately formed stator core can support consistent winding placement and magnetic alignment. The SMC structure may also offer advantages in compact motor packages where designers need to balance power density, acoustic performance, and weight.
8.3 Fresh-Air Systems and Air Purification Equipment
Fresh-air ventilators and air purifiers commonly require quiet, stable operation. Some drive motors operate at low speed with relatively high torque, making magnetic circuit design and accurate tooth geometry important.
The SMC stator core can provide a stable magnetic path for these operating conditions. Its low-noise potential and lightweight structure make it suitable for equipment installed in homes, offices, healthcare facilities, and other occupied environments.
8.4 Dehumidifiers and Portable Air Conditioners
The same technology can be extended to drive motors used in dehumidifiers, portable air conditioners, and related appliances. These products often have tight packaging requirements and may benefit from a compact, lightweight magnetic component that supports variable-speed control.
8.5 Other High-Efficiency Motor Platforms
Beyond HVAC and household appliances, SMC stator cores may be considered for selected pumps, blowers, actuators, small industrial motors, and axial-flux motor systems. Suitability depends on flux density, frequency, temperature, mechanical loading, assembly method, and customer-specific performance requirements.
9. Manufacturing Strengths of Jiande Welfine Technology Co., Ltd.
Jiande Welfine Technology Co., Ltd. was established in 2001 and operates as a high-tech enterprise integrating research and development, production, and sales. The company focuses on powder metallurgy sintering and related precision machining, with experience in powder metallurgy bushings, self-lubricating bushings, structural parts, and precision components.
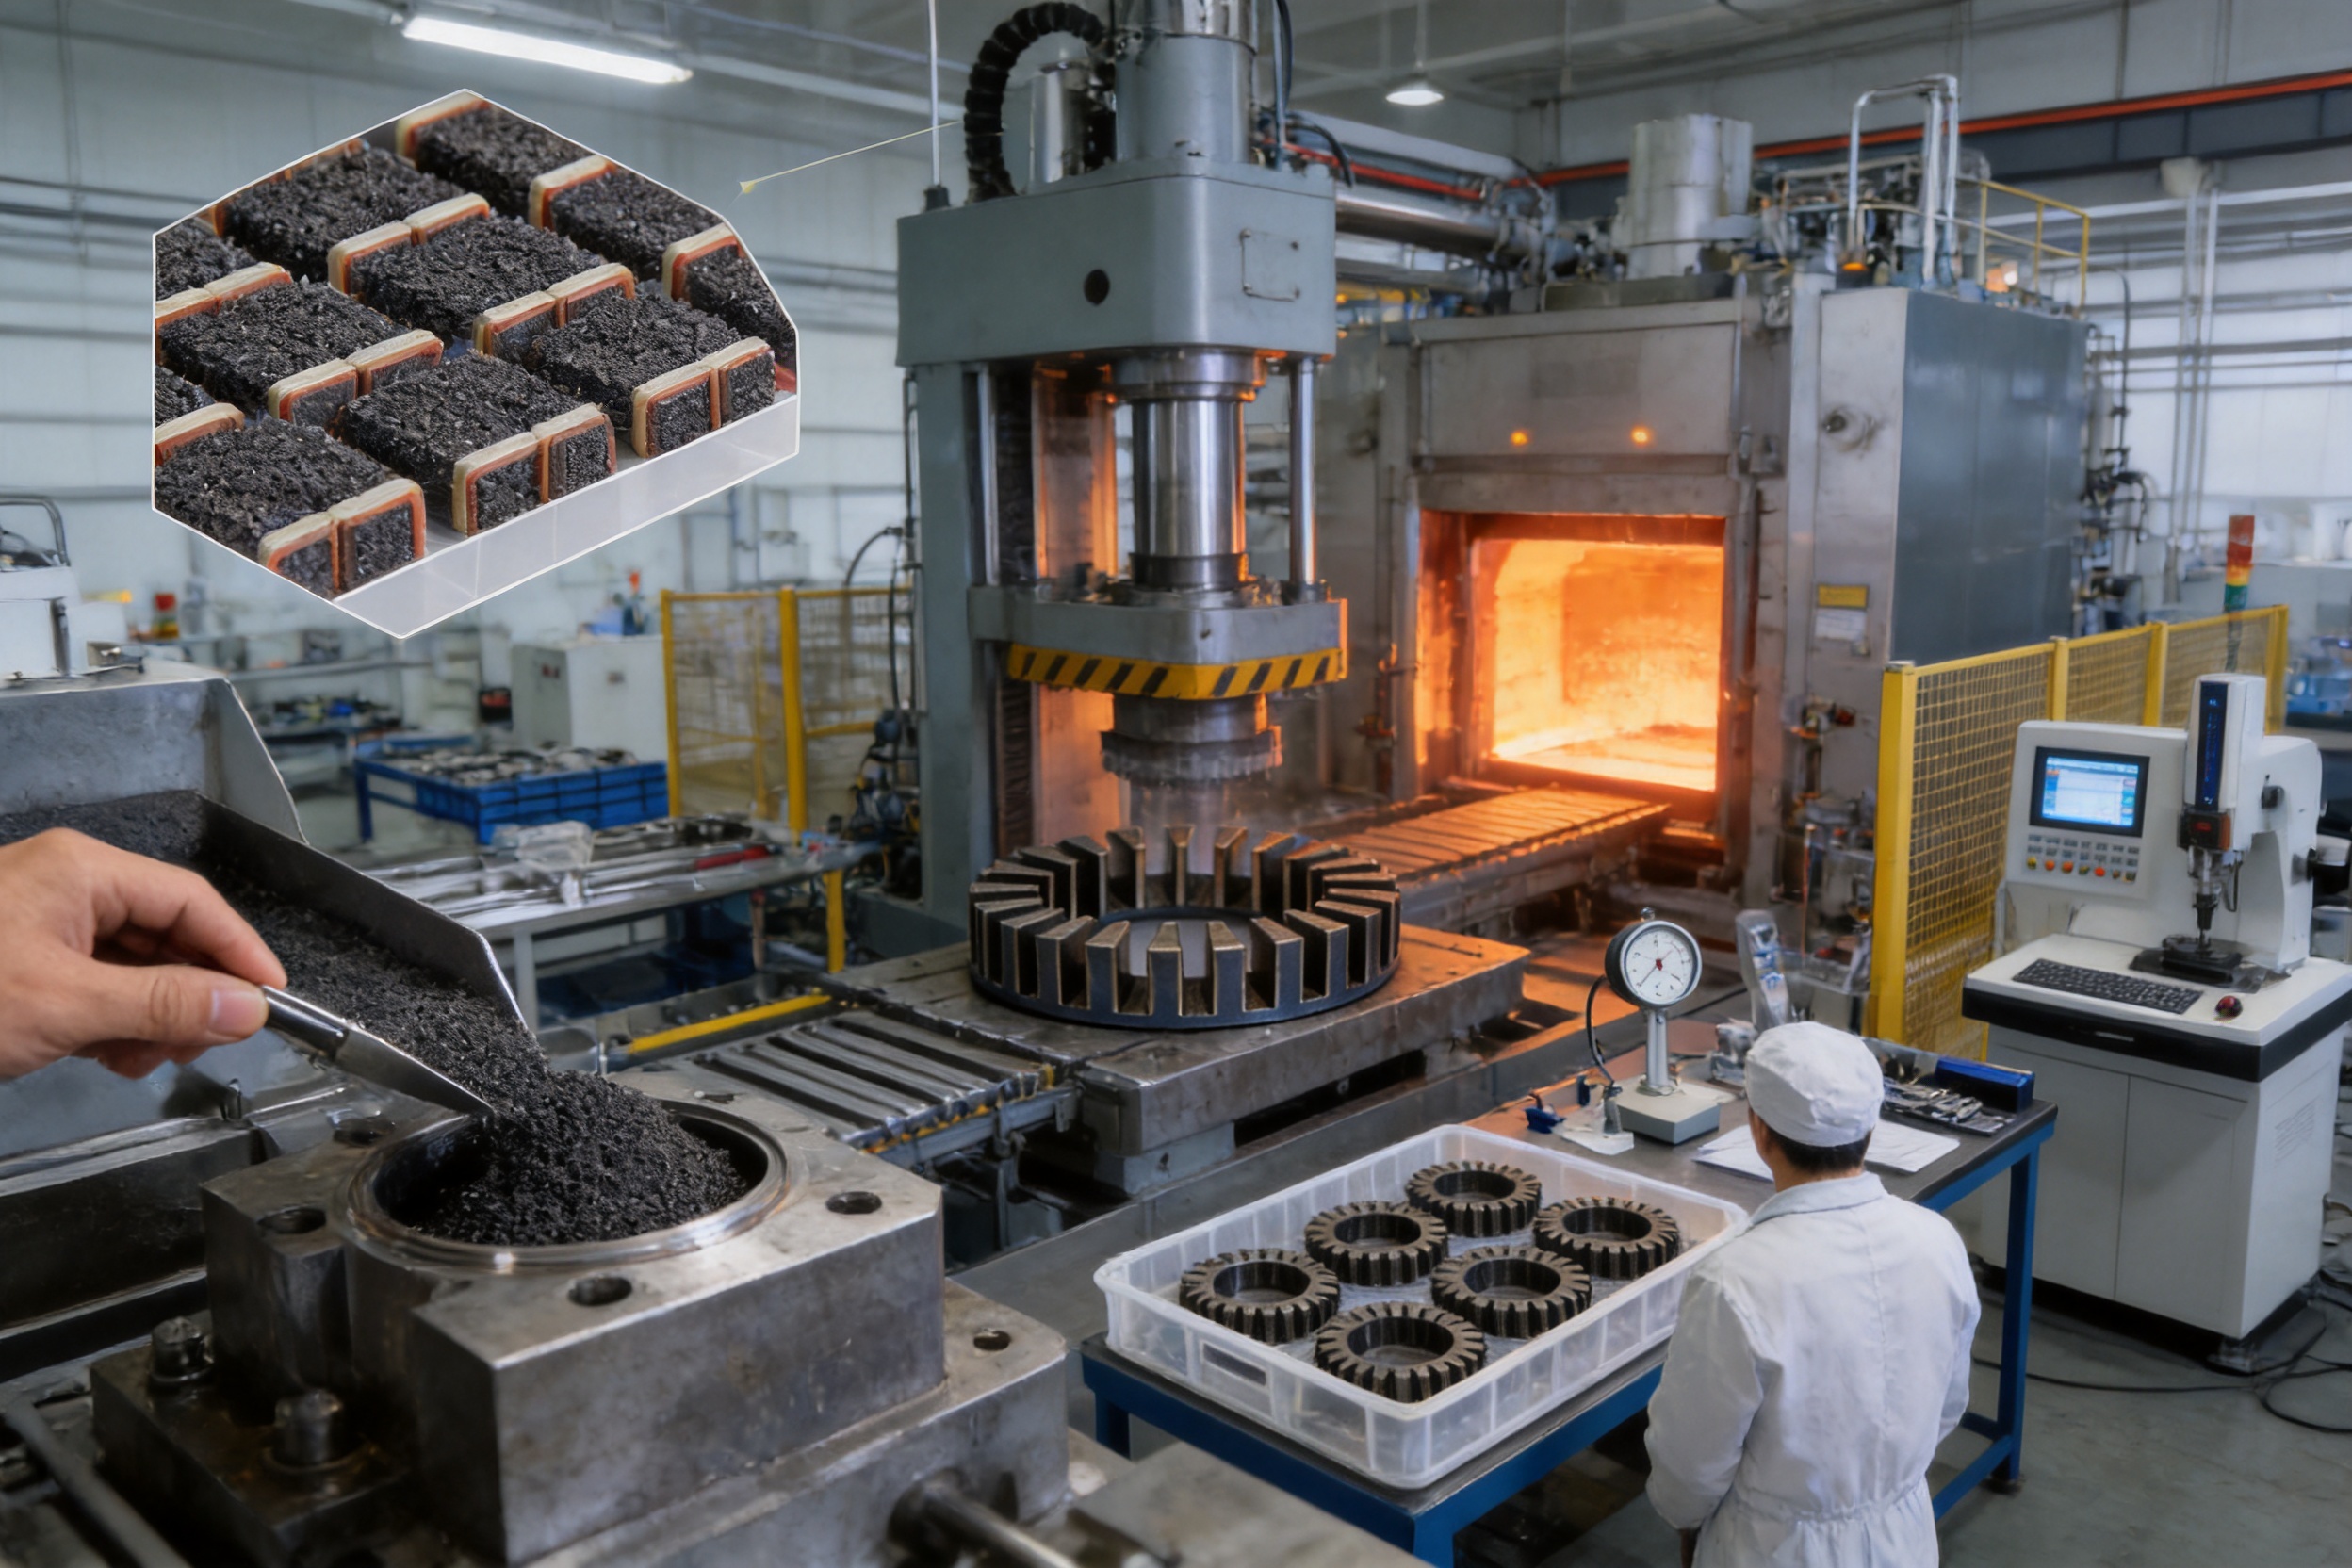
The company has a modern production base covering approximately 13,039 square meters and employs more than 150 skilled personnel. Its equipment includes high-efficiency presses, high-temperature sintering furnaces, precision forming machines, and testing equipment. This combination supports the development and manufacture of complex powder metallurgy components from initial material evaluation to finished-product inspection.
9.1 Integrated Engineering Support
SMC stator core production requires coordination between material formulation, tooling design, pressing parameters, heat treatment, post-processing, and magnetic testing. A supplier with experience in several powder metallurgy processes can evaluate these factors together rather than treating them as isolated operations.
Welfine provides OEM and ODM services based on customer drawings or samples. Engineering support may include design-for-manufacturing review, material selection, tooling assessment, dimensional analysis, prototype production, testing, and process optimization.
9.2 Quality Management
The company has passed ISO 9001:2015 and IATF 16949:2016 certifications. These quality systems support controlled documentation, process monitoring, traceability, corrective action, and continual improvement. Such systems are valuable when supplying components for motors that must perform reliably throughout extended operating cycles.
Quality control begins with incoming raw materials and continues through powder preparation, die filling, pressing, thermal processing, precision forming, inspection, packaging, and delivery. The objective is to maintain consistent dimensional, mechanical, and magnetic properties from batch to batch.
9.3 Flexible Production for OEM and ODM Programs
Different motor manufacturers may require different tooth counts, diameters, thicknesses, tolerances, magnetic properties, or assembly features. Flexible production planning allows the supplier to support prototypes, pilot batches, and stable mass production.
Welfine can adjust powder particle size distribution, coating conditions, compaction parameters, and post-processing methods to target customer-defined requirements. For example, customer programs may specify a particular permeability range, transverse rupture strength, core loss limit, operating temperature, or dimensional tolerance.
9.4 Stable Batch Supply
For appliance and HVAC programs, stable delivery is as important as initial product performance. Production scheduling, material planning, tooling maintenance, in-process inspection, and moisture-proof packaging help reduce supply interruptions and protect product quality during transportation.
10. Quality and Reliability Considerations
10.1 Dimensional Accuracy
Stator dimensions affect winding clearance, housing fit, air-gap alignment, and rotor positioning. The outer and inner diameters must remain within the approved limits, while thickness, flatness, and parallelism influence axial assembly and magnetic alignment.
Tooth profile accuracy is especially important because tooth geometry affects flux concentration, winding placement, torque ripple, and local magnetic saturation. Precision tooling and post-processing are used to maintain the specified tooth profile tolerance.
10.2 Density Distribution
Uniform density contributes to consistent magnetic performance and mechanical strength. Density gradients can arise from uneven filling, friction against the die wall, complex geometry, or inappropriate pressing parameters. Process development should therefore include density mapping or other methods of evaluating uniformity where appropriate.
10.3 Coating Integrity
Coating integrity can be evaluated through electrical resistivity, core loss, microscopic examination, thermal exposure, or other agreed methods. The selected test method should reflect the customer’s application and the expected operating frequency.
10.4 Mechanical Strength
Although the stator core is primarily a magnetic component, it must withstand production and service loads. Handling, winding insertion, press fitting, vibration, thermal expansion, and assembly forces can all impose mechanical stress. Hardness, bending strength, transverse rupture strength, and visual examination may be included in the inspection plan.
10.5 Thermal Cycling
Repeated heating and cooling can create differential expansion and contraction between the SMC core, windings, housing, adhesives, and other motor components. Thermal shock testing helps identify cracking, delamination, or dimensional instability. The stated target of no cracking after 10 cycles between 150℃ and room temperature provides a reference for thermal reliability evaluation.
11. Packaging and Delivery
SMC stator cores should be packaged to prevent moisture absorption, corrosion, impact damage, and deformation during storage and transportation. The product is supplied using moisture-proof and rust-proof independent packaging designed to reduce oxidation and contact damage.
Packaging design may be adapted according to part geometry, order quantity, shipping method, storage duration, and customer requirements. Separators, protective trays, cushioning materials, and batch labels can be used to prevent tooth damage and maintain traceability.
Delivery schedules are arranged according to order requirements and production capacity. Flexible production scheduling supports prototype orders, small engineering batches, and recurring mass-production programs. Customers should provide forecast information whenever possible so that raw materials, tooling, and production capacity can be planned effectively.
12. Customization and Product Development Process
A typical customized development project begins with the customer’s drawing, sample, three-dimensional model, motor specification, or application description. Important information includes outer and inner diameter, thickness, tooth count, tooth profile, target density, magnetic frequency range, core loss limit, mechanical loading, operating temperature, and assembly method.
The engineering team then evaluates the design for powder filling, compaction, ejection, dimensional control, heat treatment, machining, and inspection. If the geometry contains sharp corners, narrow teeth, deep cavities, or significant thickness changes, modifications may be recommended to improve manufacturability and reduce cracking risk.
Tooling is developed after the product requirements are confirmed. Prototype or trial samples are produced to evaluate density, dimensions, mechanical integrity, electrical resistivity, magnetic properties, and assembly fit. Results are reviewed against the customer’s requirements, and the process is adjusted before formal approval.
Once the design is validated, production documentation is established. This may include material specifications, process parameters, inspection plans, control plans, packaging requirements, and traceability procedures. Continuous production can then proceed under controlled conditions.
13. Selection Guidance for Buyers and Motor Designers
When selecting an SMC stator core supplier, buyers should evaluate more than the nominal material grade. The supplier should be able to demonstrate control over powder quality, coating uniformity, compaction density, thermal processing, dimensional accuracy, and magnetic testing.
Customers should clarify whether the required core loss values apply at 50 Hz, 400 Hz, or another frequency. Magnetic performance can vary significantly with frequency, flux density, waveform, temperature, and test specimen configuration. A clear testing agreement prevents misunderstandings during qualification.
Dimensional tolerances should be reviewed together with the motor assembly. For example, an inner diameter tolerance may influence rotor clearance, while flatness and parallelism may affect axial positioning. Tooth profile tolerances may influence winding insertion and electromagnetic noise.
The required mechanical properties should also be defined. A motor core used in a stationary low-load appliance may have different strength requirements from a core that experiences press fitting, high vibration, or frequent thermal cycling.
Finally, customers should consider supply capability. A suitable supplier should offer prototype support, stable batch production, quality documentation, responsive engineering communication, and packaging suitable for international transportation.
14. Frequently Asked Questions
14.1 What is an SMC stator core?
An SMC stator core is a magnetic motor component made by compacting electrically insulated iron-based powder into a three-dimensional shape. The insulation between particles helps reduce eddy current paths, while powder compaction enables complex geometries such as integrated teeth and ring-shaped structures.
14.2 How does an SMC stator core differ from a laminated silicon steel core?
A laminated silicon steel core is assembled from stacked electrical steel sheets, while an SMC stator core is formed as a three-dimensional compact from insulated magnetic particles. Laminations are highly effective in many conventional motor designs, but SMC materials provide greater freedom for three-dimensional magnetic circuits and near-net-shape forming. The best solution depends on the motor frequency, flux direction, geometry, cost target, and performance requirements.
14.3 Why is SOMALOY 700HR-3P suitable for inverter motors?
The material provides high electrical resistivity, controlled magnetic permeability, low specified core loss, and useful mechanical strength. These characteristics are relevant to inverter motors that operate across changing frequencies and loads. Final suitability must be confirmed through motor-level testing under actual operating conditions.
14.4 Can the stator core be customized?
Yes. Customization may include outer diameter, inner diameter, thickness, tooth number, tooth shape, magnetic performance, mechanical strength, surface treatment, and packaging. Jiande Welfine Technology Co., Ltd. provides OEM and ODM services based on customer drawings, samples, or technical specifications.
14.5 What information is required for a quotation?
Useful information includes a drawing or three-dimensional model, material requirement, annual or monthly quantity, target tolerances, operating temperature, frequency range, magnetic performance requirements, surface treatment, packaging method, and delivery destination. A physical sample can also support reverse engineering and feasibility evaluation.
14.6 How is the insulation coating protected during compaction?
Protection depends on the coating system, powder preparation, lubricant selection, die surface condition, compaction pressure, pressing speed, and ejection method. Properly optimized processing limits coating damage and helps maintain electrical resistivity and low core loss.
14.7 Can SMC stator cores operate at high temperature?
The stated component operating range is -40℃ to 180℃. However, the complete motor assembly includes windings, insulation, adhesives, bearings, housing materials, and other components. Therefore, the actual allowable motor temperature must be determined through system-level thermal validation.
14.8 What applications are suitable for this product?
Potential applications include household inverter air conditioner motors, commercial HVAC fan motors, fresh-air systems, air purification equipment, dehumidifiers, portable air conditioners, and selected high-efficiency or axial-flux motor platforms.
14.9 Does the company support small trial orders?
Production arrangements depend on tooling, material availability, geometry, and customer requirements. The company can discuss prototype development, pilot batches, and recurring production schedules as part of an OEM or ODM program.
14.10 How should finished stator cores be stored?
Finished products should be kept in clean, dry, temperature-controlled or humidity-controlled storage where practical. They should remain in their protective packaging until assembly and should be protected from impact, condensation, corrosive chemicals, and excessive stacking pressure.
15. Conclusion
The SMC stator core made from SOMALOY 700HR-3P provides a practical solution for motor manufacturers seeking lower core loss, three-dimensional magnetic design capability, accurate tooth geometry, and lightweight construction. Its insulated particle structure helps control eddy current loss, while powder metallurgy enables complex ring-shaped toothed components to be formed efficiently.
The stated product combines a saturation magnetic induction of at least 1.5 T, initial permeability of at least 300 μ₀, maximum permeability of at least 1000 μ₀, controlled core loss, high electrical resistivity, and mechanical strength suitable for demanding motor assemblies. Dimensional specifications such as a Φ100.0 mm outer diameter, Φ65.0 mm inner diameter, 10.0 mm thickness, 18 teeth, and tight flatness and parallelism targets support accurate integration with windings and housings.
Jiande Welfine Technology Co., Ltd. strengthens this product offering through more than 20 years of powder metallurgy experience, a 13,039-square-meter manufacturing base, modern pressing and sintering equipment, precision post-processing capabilities, ISO 9001:2015 and IATF 16949:2016 certification, and OEM/ODM engineering support. By controlling powder preparation, insulation coating, compaction, thermal processing, inspection, and packaging, the company can provide customized magnetic components for stable and efficient motor production.
For motor designers, HVAC manufacturers, and purchasing teams, the SMC stator core is most valuable when it is evaluated as part of the complete motor system. Proper validation of magnetic performance, thermal behavior, mechanical strength, dimensional fit, noise, vibration, and long-term reliability will ensure that the selected core delivers its full potential in the intended application.
References
1. SOMALOY 700HR-3P material information and technical data supplied for the product specification.
2. Powder Metallurgy Components: Manufacturing Principles and Applications, industry reference material.
3. Soft Magnetic Composites for Electrical Motor Applications, technical literature on insulated iron powder materials.
4. Electrical Steels and Magnetic Core Materials, reference material covering core loss, permeability, coercivity, and magnetic circuit design.
5. ISO 9001:2015, Quality Management Systems—Requirements.
6. IATF 16949:2016, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
7. General industry practices for powder particle size analysis, compaction control, thermal processing, dimensional inspection, and magnetic testing.
Product: SMC Stator Core (SOMALOY 700HR-3P)
Related products
-
-
Description: 79.5×62×7.3mm copper-based brake pad with 4-hole design. Density 6.2g/cm³, weight 195g. Free from graphite segregation, cracks, and defects. Ideal for heavy-duty industrial braking system...
See Details -
Product Description: High-precision powder metallurgy part (S14*7*10) made of iron material from Jiande Wefine, customized PM components with strict tolerance control.
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Privacy Custom Self-lubricating Sintered Bushing Manufacturers
