E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Shen Yiruo — Senior After-Sales Service Manager / Powder Metallurgy Structural Components for Washing Machine Clutch and Transmission Systems
Powder Metallurgy Structural Components for Washing Machine Clutch and Transmission Systems
 2026.10.14
 Shen Yiruo — Senior After-Sales Service Manager
Content
- 1 Product Overview
- 2 Functional Role in Washing Machines
- 3 Powder Metallurgy Manufacturing Process
- 4 Key Product Advantages
- 5 Advantages Compared with Conventional Manufacturing Methods
- 6 Design Considerations for OEM and ODM Projects
- 7 Manufacturing and Engineering Strengths
- 8 Customization and Project Development
- 9 Applications in Washing Machine Systems
- 10 Quality, Reliability, and Supply Considerations
- 11 Economic and Environmental Benefits
- 12 Technical Support for International Customers
- 13 Q&A
- 13.1 What are these powder metallurgy structural components used for?
- 13.2 Which materials are available?
- 13.3 How are the components manufactured?
- 13.4 Why is powder metallurgy suitable for washing machine parts?
- 13.5 What is the purpose of the black oxide treatment?
- 13.6 Can the spline and serration profiles be customized?
- 13.7 Can the components be supplied in different sizes?
- 13.8 What quality certifications support production?
- 13.9 Can samples be tested before mass production?
- 13.10 What information should a customer provide for a quotation?
- 13.11 How does powder metallurgy compare with machined steel?
- 13.12 Is blackening a replacement for lubrication?
- 14 Conclusion
- 15 References
- 16 Product: Powder Metallurgy Structural Components for Washing Machines
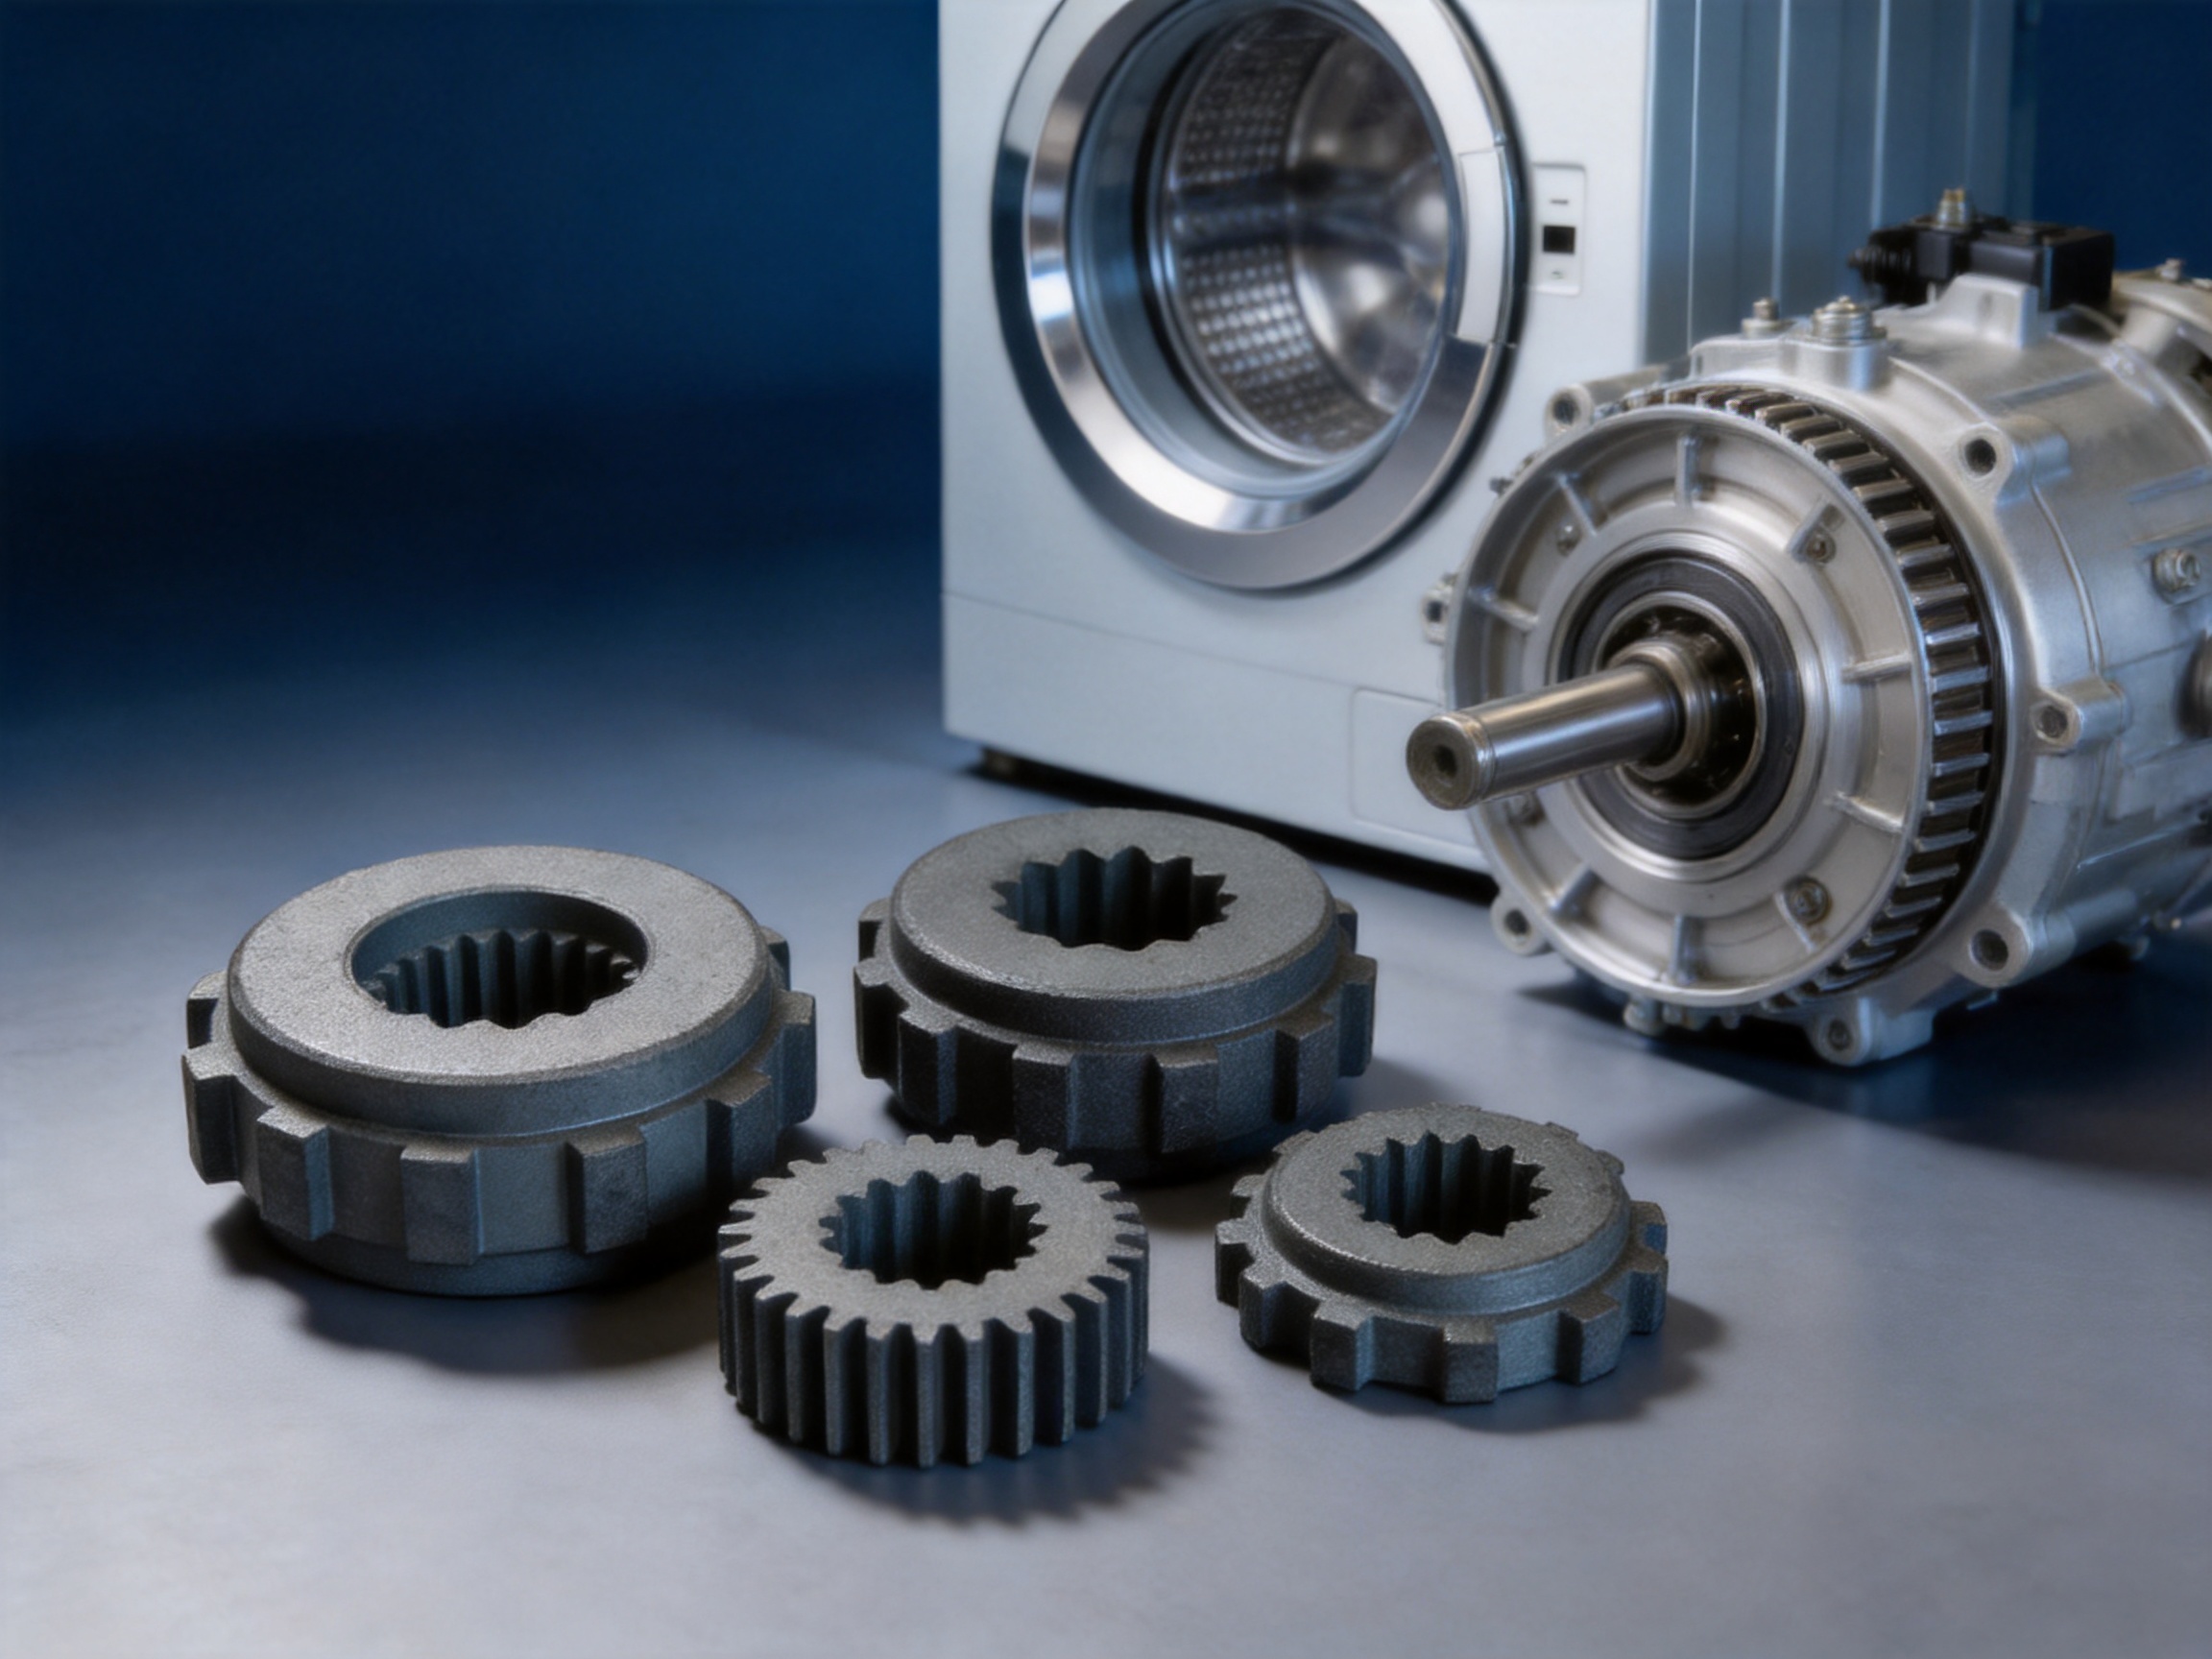
Modern washing machines rely on compact, durable, and precisely fitted transmission components to perform repeated washing, rinsing, and spinning cycles. Among the most important parts in these systems are the structural components used in clutch assemblies, torque-transfer mechanisms, and transmission units. These components must transmit rotational force, engage and disengage reliably, withstand repeated load changes, and maintain dimensional accuracy throughout a long operating life.
Powder metallurgy structural components provide an efficient solution for these demanding applications. Produced from iron-based powder metallurgy alloys through compaction, high-temperature sintering, and blackening treatment, these parts combine strength, wear resistance, dimensional stability, and manufacturing efficiency. Their near-net-shape production method also makes it possible to form complex internal splines, serrations, and external gear-like profiles with limited secondary machining.
For washing machine manufacturers, the value of these components extends beyond the individual part. A well-designed sintered structural component can help improve clutch engagement, stabilize torque transmission, reduce production waste, support consistent assembly, and lower total manufacturing costs. It can also be customized to match the dimensions, profiles, material requirements, and performance conditions of a particular washing machine model.
Powder Metallurgy Structural Components for Washing Machines
Product Overview
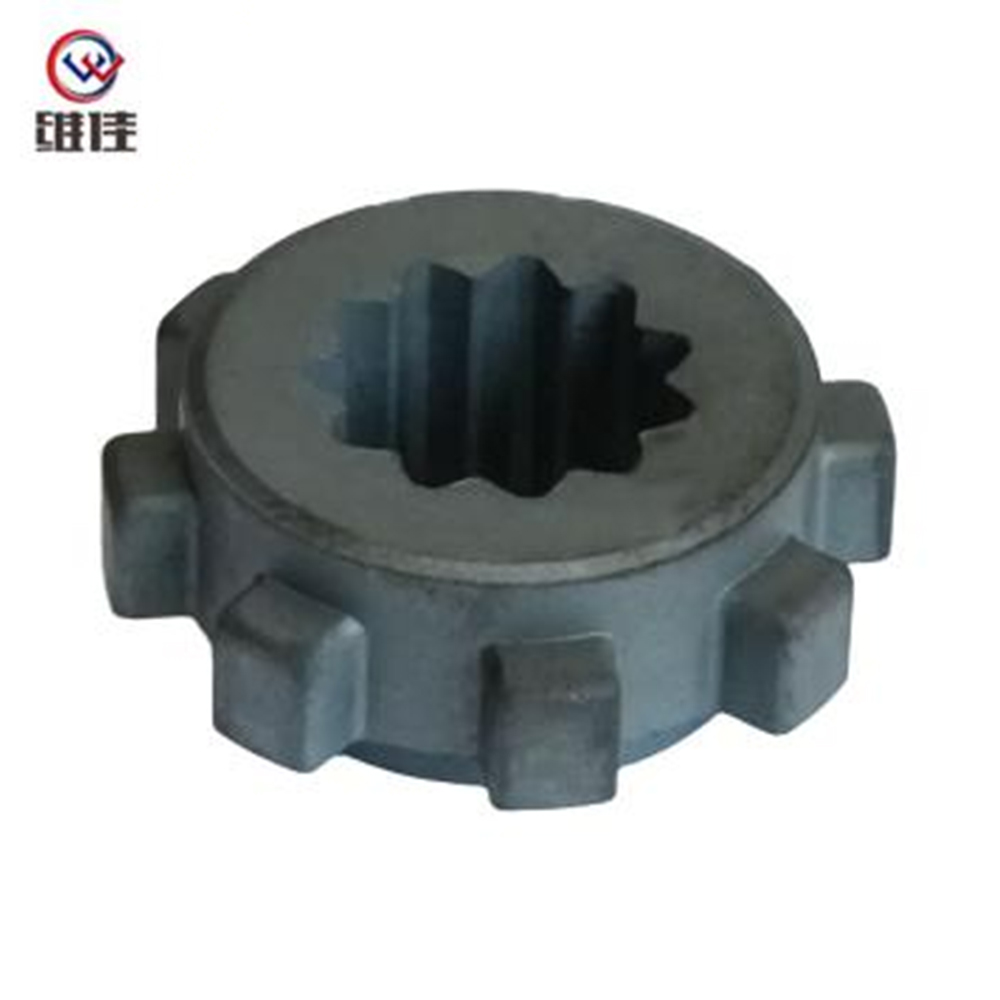
These powder metallurgy structural components are iron-based parts developed for washing machine clutch assemblies and transmission systems. They are manufactured by compacting blended metal powders in a precision die, sintering the compacted shape at high temperature, and applying a black oxide surface treatment. The resulting component is designed to operate in mechanisms where repeated torque transmission and mechanical engagement are required.
The typical material options include iron-copper-carbon and iron-nickel-carbon powder metallurgy alloys. Material selection can be adjusted according to the required strength, hardness, wear resistance, dimensional stability, and operating conditions. The use of alloyed iron powders allows the component to achieve a balance between mechanical performance and cost efficiency.
The inner profile may be formed with splines or serrations that engage with a mating shaft or transmission element. The outer profile may contain serrations, gear-like teeth, or other engagement features used to connect with clutch mechanisms. These profiles are created during compaction, allowing complex geometry to be produced in a repeatable and economical manner.
Parameter |
Typical Specification |
Product Type |
Iron-based powder metallurgy structural component |
Primary Materials |
Fe-Cu-C or Fe-Ni-C powder metallurgy alloy |
Manufacturing Process |
Powder blending, precision compaction, high-temperature sintering, and blackening |
Surface Treatment |
Black oxide coating for improved corrosion resistance and surface performance |
Inner Geometry |
Splined or serrated bore for torque transmission |
Outer Geometry |
Serrated or geared profile for clutch engagement |
Application |
Washing machine clutch assemblies and transmission systems |
Production Scope |
Custom dimensions, profiles, materials, and OEM/ODM configurations |
The components can be supplied in different sizes and configurations according to the design requirements of the washing machine. Engineering support is available for drawing review, prototype development, sample testing, and production scaling.
Functional Role in Washing Machines
A washing machine transmission system must perform several different functions during one operating cycle. During washing, the drum or agitator may rotate at a relatively low speed while changing direction repeatedly. During spinning, the system must support higher-speed rotation and maintain stable torque transmission. Between these operating conditions, the clutch mechanism may engage or disengage different drive paths.
Structural components within the clutch and transmission assembly help transfer the motor’s rotational force through the appropriate mechanical interfaces. The inner spline or serration transmits torque between the component and a shaft or mating part. The outer profile can engage a clutch ring, gear, or other transmission element. Because the parts are integrated into a mechanical engagement system, profile accuracy and dimensional consistency are essential.
The component must also withstand mechanical stress caused by starting, stopping, reversing, acceleration, deceleration, and changes in the load applied by the rotating drum. These forces are repeated throughout the service life of the appliance. If the engagement profiles wear excessively or the component loses its dimensional stability, the clutch may become noisy, slip, engage incompletely, or transfer torque inefficiently.
Powder metallurgy structural components are particularly suitable for these conditions because the manufacturing process can produce a dense, stable, and accurately shaped part with the required engagement features. The process also supports consistent production across large batches, which is important for appliance manufacturers that require reliable interchangeability.
Powder Metallurgy Manufacturing Process
Powder Selection and Alloy Design
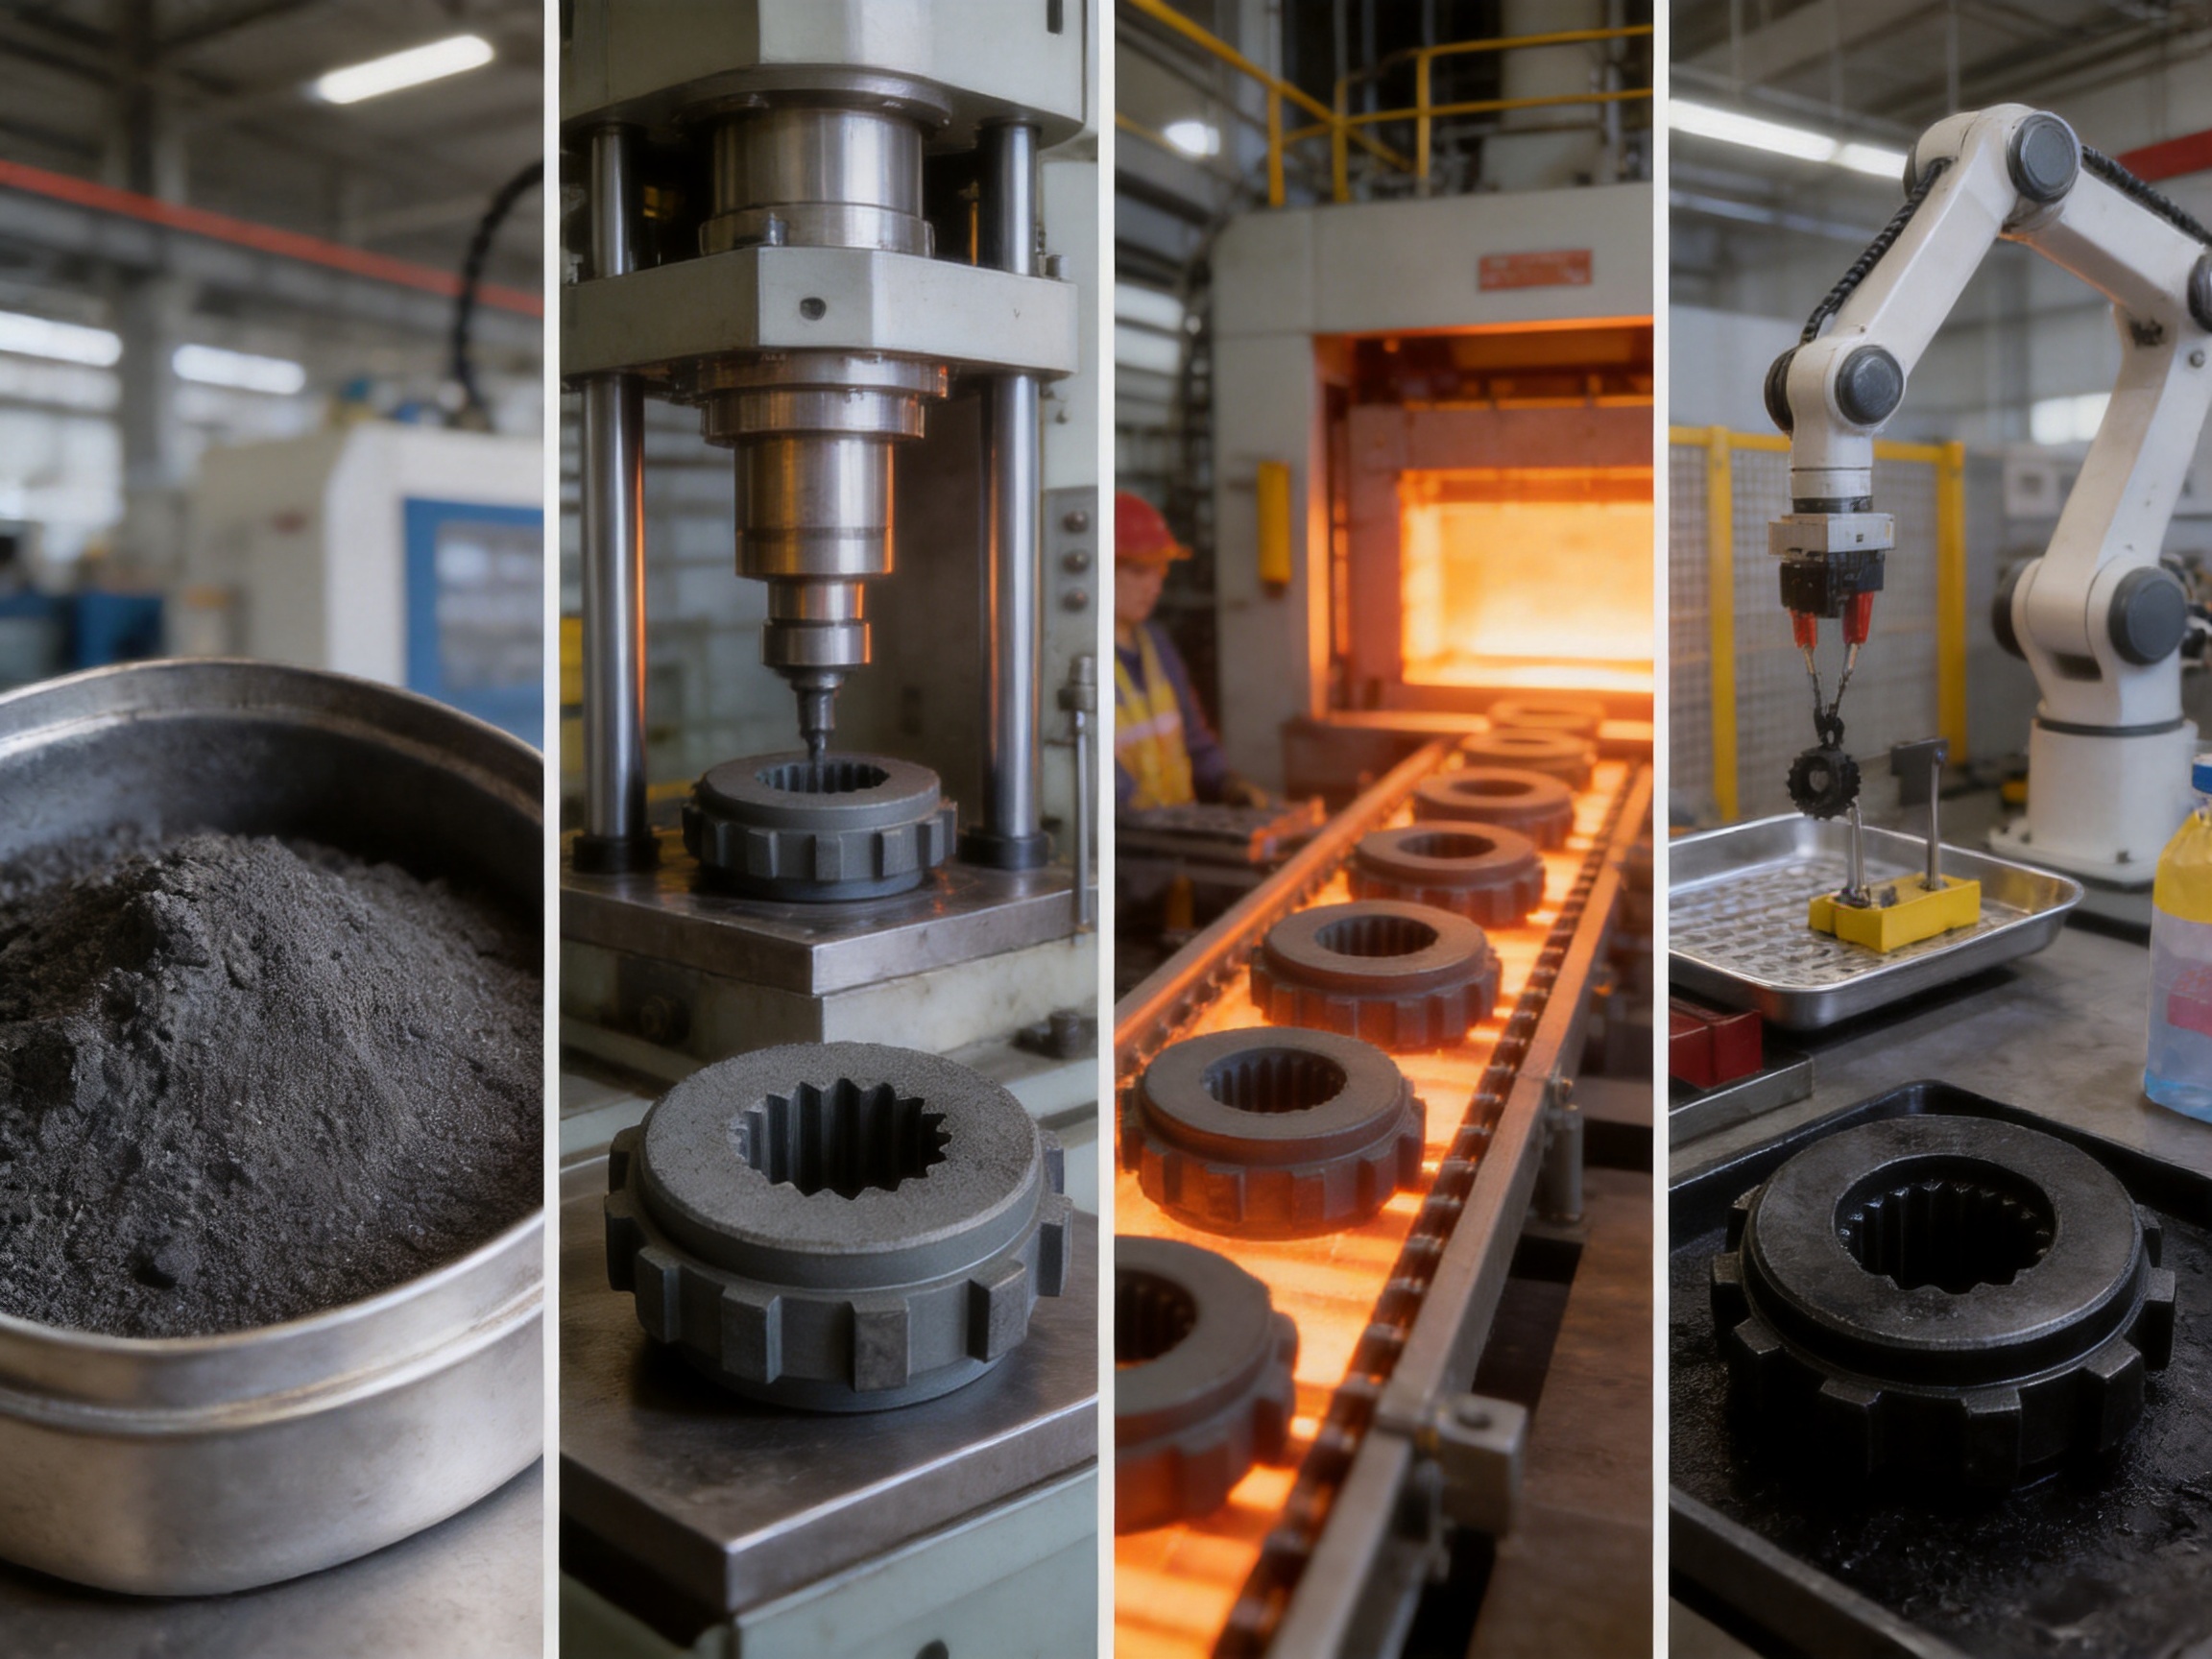
The manufacturing process begins with the selection of an appropriate iron-based powder mixture. Fe-Cu-C and Fe-Ni-C systems are commonly used because copper, nickel, and carbon can modify the strength, hardness, toughness, and dimensional behavior of the iron matrix. The final composition is selected according to the design requirements of the component and the intended operating environment.
Powder characteristics influence the filling behavior of the die, the compacting response, the final density, and the mechanical properties after sintering. Particle size distribution, apparent density, flowability, compressibility, and lubricant content must be controlled carefully. A stable powder blend supports reliable die filling and helps reduce variation between individual parts.
For customized projects, the material formulation may be adjusted after reviewing the component geometry, load conditions, mating parts, required surface properties, and production volume. This engineering approach is more effective than selecting a material solely by nominal chemical composition, because the finished performance depends on the combined effects of alloy design, density distribution, sintering conditions, and surface treatment.
Precision Die Filling and Compaction
After powder preparation, the blend is placed into a forming die. A high-efficiency press applies controlled pressure to compact the powder into the required shape. The die is designed to form the component’s external contour, internal bore, spline configuration, serration pattern, and other functional features.
Compaction is one of the most important stages because it determines the green shape and establishes the initial density distribution. Pressing conditions must be selected carefully for components with different wall thicknesses, stepped profiles, internal teeth, or complex engagement surfaces. Proper tooling design helps ensure that the powder fills the die uniformly and that the compact can be removed without cracking or distortion.
One significant advantage of powder metallurgy is that many features can be formed during compaction rather than machined afterward. Internal splines and external serrations may be created directly by the forming tool. This reduces material removal, shortens production time, and limits the number of secondary operations required.
Precision compaction also supports repeatability. When powder characteristics, tooling conditions, press settings, and process controls are stable, the resulting green compacts have consistent dimensions and predictable behavior during sintering.
High-Temperature Sintering
The compacted parts are transferred to a high-temperature sintering furnace. During sintering, the particles bond together through solid-state diffusion. The controlled thermal cycle removes lubricants, promotes metallurgical bonding, and develops the mechanical strength of the component.
Temperature, atmosphere, heating rate, soaking time, and cooling conditions all influence the final properties. The furnace atmosphere must be managed to limit unwanted oxidation and support the required chemical reactions within the material. A well-controlled sintering process improves structural integrity and helps maintain a stable relationship between density, strength, hardness, and dimensional change.
Sintering is also important for the accuracy of the internal and external profiles. Although some dimensional change is expected as the compact develops its final structure, predictable furnace control allows this change to be compensated for in the tooling and process design. This contributes to reliable production of components that fit correctly within washing machine clutch and transmission assemblies.
The final density can be influenced by the compaction pressure, powder formulation, geometry, and sintering cycle. Higher-density regions are especially important around torque-transmission features, splines, serrations, and areas exposed to contact stress. Process engineering is therefore required to balance dimensional accuracy with the mechanical performance needed for the application.
Blackening Treatment
Following sintering, the components may receive a black oxide or blackening treatment. This process forms a dark oxide layer on the surface and provides several practical benefits. It improves the part’s resistance to atmospheric corrosion, supports anti-rust performance during storage and assembly, and creates a uniform appearance.
Blackening can also contribute to improved surface behavior in applications involving repeated contact and sliding. The treatment does not replace the need for correct material selection or adequate lubrication, but it can complement the inherent properties of the sintered alloy. In washing machine transmission environments, where the component may be exposed to humidity and periodic temperature changes, surface protection is an important part of product reliability.
The black oxide finish also gives the parts a consistent dark appearance that can help distinguish treated components during assembly and quality inspection. The treatment is applied as part of a controlled production route rather than as an informal finishing step, allowing surface quality to be monitored together with dimensional and mechanical characteristics.
Inspection and Quality Verification
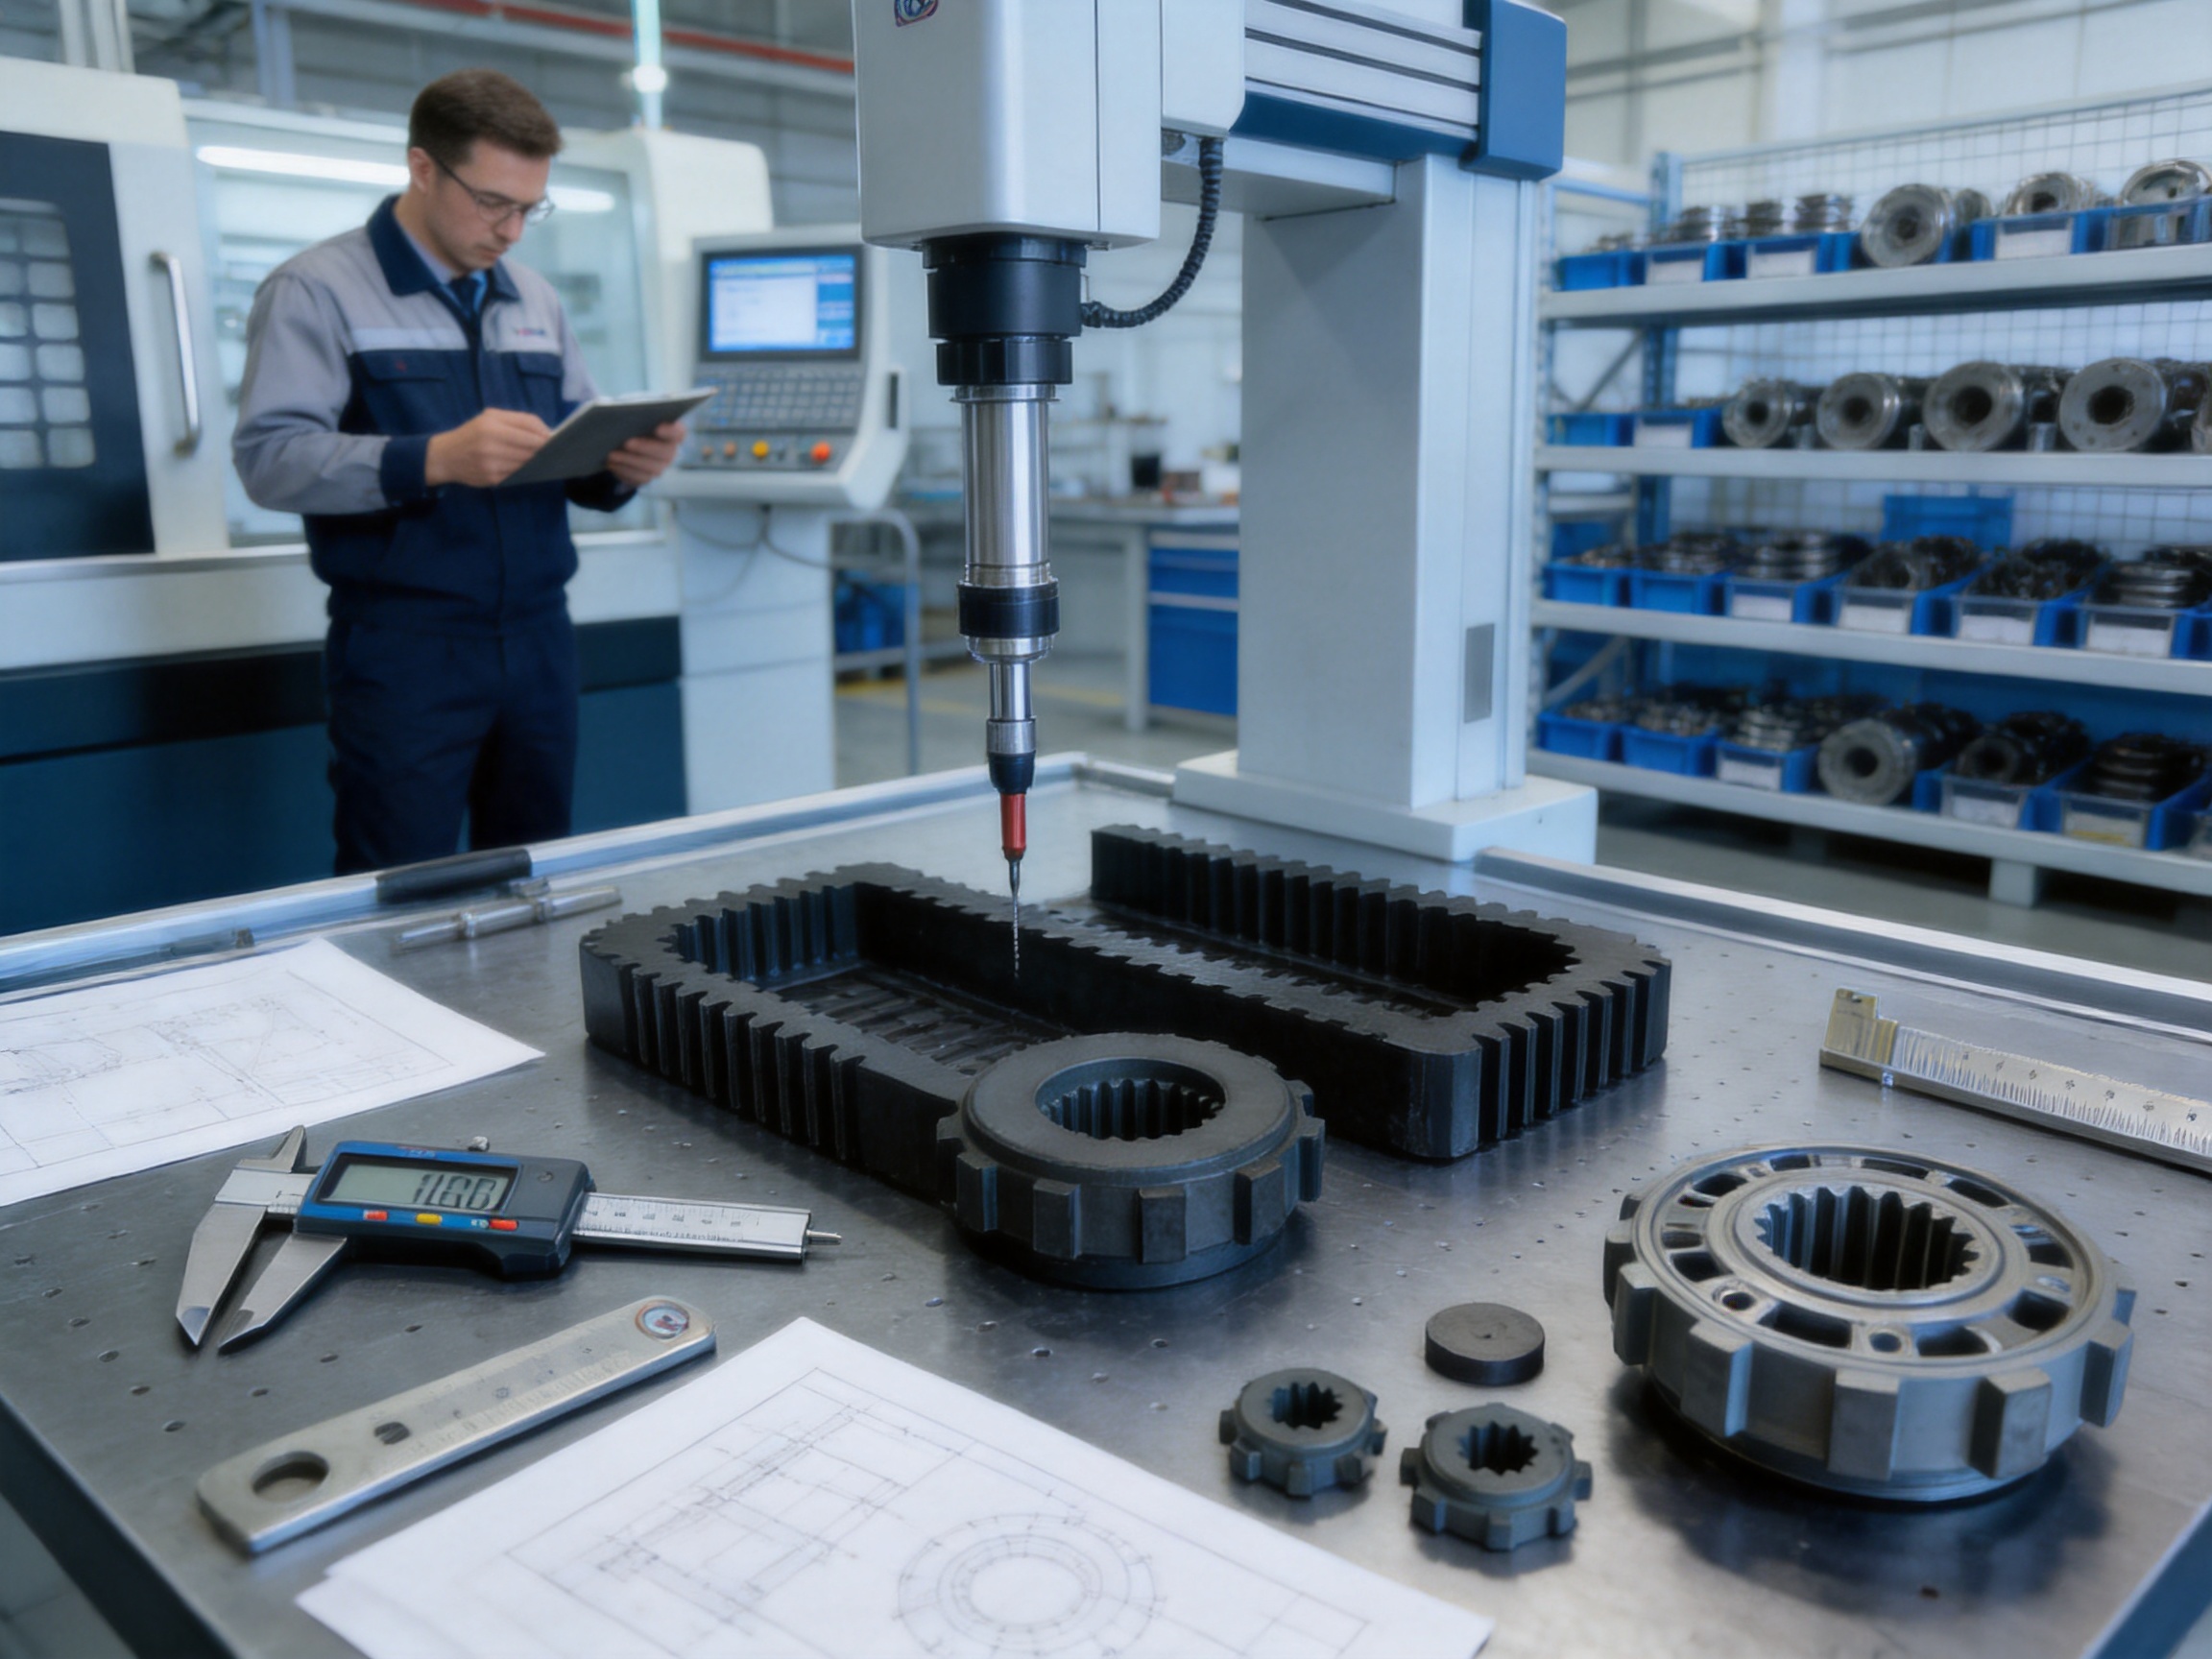
Quality assurance extends across the entire production process. Incoming powder materials are evaluated for consistency, while production parameters are monitored during compaction and sintering. Finished parts are inspected for critical dimensions, profile accuracy, surface condition, appearance, and mechanical properties.
Dimensional inspection may include measurements of the outer diameter, inner bore, thickness, tooth or serration geometry, flatness, concentricity, and other customer-defined features. Depending on the project, density, hardness, tensile strength, dimensional change, and wear-related properties may also be evaluated.
Inspection methods are selected according to the component’s function. A simple visual check may confirm the black oxide appearance, while precision gauges, measuring equipment, and specialized fixtures may be used to verify the spline or serration profile. Samples can be tested during prototype development before a customized design moves to mass production.
A documented quality management system supports process traceability and continuous improvement. The manufacturing organization described for these products operates with ISO 9001:2015 and IATF 16949:2016 certifications, providing a structured framework for quality planning, process control, corrective action, and customer-focused production.
Key Product Advantages
Near-Net-Shape Manufacturing
Near-net-shape production is one of the most important advantages of powder metallurgy. Instead of starting with a larger billet and removing a substantial amount of material, the component is formed close to its final geometry during compaction. This approach reduces scrap, decreases machining requirements, and improves material utilization.
For structural components with internal and external engagement profiles, near-net-shape manufacturing can be especially valuable. Conventional machining may require multiple operations to produce an inner spline, outer serration, stepped section, and controlled face geometry. Powder metallurgy can form many of these features in one compaction operation, reducing the complexity of the downstream process.
Lower material consumption can improve cost efficiency while also supporting more sustainable production. Reduced machining means less cutting waste, lower tool consumption in certain applications, and shorter processing routes. These benefits are most noticeable when the component is produced in medium or high volumes.
Complex Geometry and Integrated Functional Features
Washing machine clutch components often require more than a simple cylindrical shape. They may contain internal splines, external serrations, shoulders, recesses, and other profiles that must align with mating parts. Powder metallurgy tooling can integrate many of these features into the compact.
Forming the geometry directly can improve consistency between the inner and outer profiles. It can also reduce the risk of errors associated with multiple machining setups. When several features are created in one controlled forming operation, their relationship to one another can be maintained more efficiently.
Complex geometry does require careful engineering. The component must be designed to accommodate powder filling, compaction direction, ejection, sintering shrinkage, and any necessary secondary operations. An experienced powder metallurgy manufacturer can review the design and recommend modifications that improve manufacturability without compromising the function of the part.
Stable Mechanical Performance
Iron-based powder metallurgy alloys can provide the mechanical strength required for repeated torque transmission. Fe-Cu-C and Fe-Ni-C systems are suitable for developing components with a balanced combination of strength, hardness, wear resistance, and dimensional stability.
Uniform process control helps maintain consistent properties from batch to batch. This is important for washing machine production because a large number of identical components may be assembled into different appliance models. Stable mechanical performance helps reduce variation in clutch behavior and contributes to predictable product quality.
The final performance depends on density and geometry as well as chemical composition. For this reason, the component should be developed through a complete process assessment rather than by material substitution alone. The powder formulation, compaction strategy, sintering cycle, and blackening treatment must work together as one manufacturing system.
Wear and Corrosion Resistance
Clutch and transmission components operate under repeated contact, engagement, and torque loading. Wear resistance is therefore essential. The sintered iron-based structure provides the base mechanical performance, while the black oxide layer supports surface protection and anti-rust behavior.
The combination is useful in the humid environment associated with household washing machines. Although the final operating conditions depend on the appliance design, the surface treatment provides an additional barrier against corrosion during storage, assembly, and service.
Wear resistance is also influenced by the mating components, lubrication conditions, surface pressure, alignment, and operating temperature. Correct design of the spline and serration geometry is therefore necessary to achieve the full benefit of the material and treatment. Customized development can address these factors before production begins.
Dimensional Stability and Assembly Compatibility
Dimensional stability is critical when a component must fit inside a clutch or transmission assembly. Excessive variation may create interference, looseness, misalignment, noise, or poor torque transfer. Powder metallurgy production can provide repeatable dimensions when tooling, compaction, sintering, and inspection are carefully controlled.
Stable dimensions also support efficient assembly. Components that conform reliably to drawing requirements can reduce manual adjustment and minimize the risk of assembly-line interruptions. For OEM customers, consistent interchangeability is especially important because the same component may be installed in a large number of appliances.
Dimensional control begins during design. The manufacturer can review tolerances, identify critical-to-function features, and recommend suitable measurement methods. This helps ensure that the finished specification reflects both the performance requirement and the practical capability of the selected manufacturing process.
Cost Efficiency for Volume Production
Powder metallurgy is well suited to repeated production because the tooling creates a consistent shape with limited material waste. Once the process has been developed and validated, the same production route can be used to manufacture large quantities of components with a high degree of repeatability.
Cost efficiency results from several factors, including reduced scrap, fewer machining operations, shorter cycle times, and reduced labor associated with complex feature production. The economics are particularly attractive when the design can take advantage of near-net-shape forming and when the component is required in stable production volumes.
Lower production cost does not mean that quality is sacrificed. On the contrary, a well-controlled powder metallurgy process can combine competitive pricing with defined material properties, controlled dimensions, and documented inspection. This balance is a major reason for using sintered structural components in appliance manufacturing.
Advantages Compared with Conventional Manufacturing Methods
Compared with Machining from Solid Stock
Machining a washing machine clutch component from solid steel can provide high dimensional accuracy, but it may involve substantial material removal. Internal splines and external serrations can require broaching, hobbing, milling, turning, or other operations. Multiple setups increase processing time and may introduce cumulative dimensional variation.
Powder metallurgy forms much of the required geometry during compaction. This can reduce cutting waste and simplify the production route. It is especially advantageous when the component contains repeated teeth or serrations that would otherwise require dedicated machining operations.
Machining may remain appropriate for very low quantities, special materials, or features that cannot be formed effectively in a die. However, for stable OEM production, powder metallurgy can provide a more economical and consistent solution.
Compared with Forging
Forging can produce strong components with excellent structural integrity, but complex internal profiles may require subsequent machining. Forging dies can also involve significant tooling investment, and the process may generate flash or require additional trimming.
Powder metallurgy offers a different balance of properties and manufacturing efficiency. It can form intricate profiles directly while using a controlled quantity of powder. For components that do not require the full directional grain structure associated with certain forged designs, sintered alloys can provide adequate performance at a competitive cost.
The appropriate process depends on the load, geometry, quantity, tolerance, and performance requirements. A technical comparison should consider total manufacturing cost and finished-part performance rather than material price alone.
Compared with Cast Components
Casting is useful for producing certain complex shapes, but cast structures may contain porosity, dimensional variation, or surface conditions that require further processing. Thin engagement features and small internal profiles may also be difficult to control economically in some casting processes.
Powder metallurgy offers controlled powder composition and the ability to form compact, repeatable profiles. The sintering process produces a metallurgically bonded structure, while the blackening treatment provides a consistent surface finish. These characteristics make the process suitable for small and medium-sized structural parts used in high-volume appliances.
Design Considerations for OEM and ODM Projects
Geometry and Profile Requirements
The inner spline or serration must match the mating shaft or transmission element. Important considerations include the number of teeth, tooth form, pressure angle where applicable, bore size, engagement length, fit, and torque requirement. The outer profile must similarly match the clutch ring, gear, or engagement mechanism.
Designers should identify which surfaces transmit torque and which surfaces primarily provide positioning or support. Critical engagement surfaces may require tighter controls than non-functional exterior surfaces. The component design should also consider the direction of compaction and the ability of the tooling to form each feature correctly.
Density Distribution
Different areas of the component may experience different loads. Spline roots, serration tips, shoulders, and bearing contact areas may require particular attention during design and process development. A suitable compaction strategy can help achieve an appropriate density distribution throughout the part.
Uniform density is desirable, but complete uniformity is not always possible in a complex geometry. Engineering analysis is used to identify potential weak areas, reduce density gradients, and avoid defects such as cracks, lamination, or distortion.
Tolerances and Sintering Behavior
All powder metallurgy parts experience some dimensional change during sintering. The amount and direction of change depend on the material, density, geometry, furnace conditions, and tooling design. These factors are taken into account when creating the compaction die.
OEM drawings should distinguish between critical and non-critical dimensions. Tolerances that are tighter than necessary may increase tooling and inspection costs without improving assembly performance. Conversely, insufficient control of an engagement feature may result in noise, looseness, or torque-transfer problems. Early technical communication helps establish practical and functional tolerances.
Surface Treatment and Operating Environment
Blackening is suitable when a dark, uniform finish and improved corrosion resistance are required. The treatment should be considered together with storage conditions, humidity, lubrication, contact pressure, and the materials used for mating components.
If a specific corrosion test, appearance requirement, or friction condition applies, it should be defined during the quotation and development stage. This allows the production team to confirm that the proposed material and finishing route are appropriate for the complete application.
Manufacturing and Engineering Strengths
The supplier behind these products was established in 2001 and focuses on powder metallurgy sintering, self-lubricating bushings, structural parts, and related precision components. More than two decades of industry experience provide a practical foundation for developing parts according to customer drawings, samples, and application requirements.
The production base covers approximately 13,039 square meters and is equipped with high-efficiency presses, high-temperature sintering furnaces, precision forming machines, and inspection equipment. This combination of production and testing resources supports both prototype development and volume manufacturing.
More than 150 skilled employees contribute to engineering, production, quality control, project coordination, and customer support. A multidisciplinary team is important for powder metallurgy because product performance depends on the relationship between design, powder formulation, tooling, compaction, sintering, finishing, and inspection.
The company provides OEM and ODM services for customers that require customized dimensions, inner and outer spline configurations, material compositions, or surface treatments. Engineering personnel can review drawings, analyze manufacturability, produce samples, and support the transition from prototype to mass production.
Quality management is supported by ISO 9001:2015 and IATF 16949:2016 certifications. These systems encourage controlled procedures, documented records, process monitoring, nonconformance management, corrective action, and continual improvement. For customers in the appliance industry, such systems help create confidence in product consistency and supply stability.
Customization and Project Development
Customization begins with the customer’s technical information. This may include a two-dimensional drawing, three-dimensional model, physical sample, material specification, assembly description, annual demand, and performance target. If some information is not yet available, the component can be evaluated based on photographs, measurements, or a description of the clutch system.
During the design review, engineers consider the geometry, pressing direction, wall thickness, profile complexity, expected load, wear condition, and surface treatment. They may recommend changes that improve powder filling or reduce the risk of cracking during ejection. Such recommendations can lower production risk and improve the stability of the final process.
Prototype samples allow the customer to check dimensions, fit, engagement, appearance, and initial operating behavior. Where required, samples can be tested in the customer’s assembly or evaluated through laboratory measurements. Feedback from sample testing is then used to refine the tooling, material, or process conditions.
After approval, production is scaled according to the required quantity and delivery schedule. Process documentation, inspection plans, and quality requirements can be established before regular production begins. This creates a controlled transition from development to repeat supply.
Applications in Washing Machine Systems
Clutch Engagement Components
The most direct application is in the clutch mechanism that switches between operating modes. The component’s inner and outer profiles allow it to engage with selected transmission elements. Accurate geometry helps the clutch engage completely and disengage when required.
A reliable engagement component can contribute to smoother operation, reduced mechanical noise, and stable torque transfer. The exact behavior depends on the overall clutch design, but the dimensional accuracy and wear resistance of the structural part are essential contributors.
Transmission Torque Transfer
In the transmission system, the component transfers rotational force between shafts, gears, and other drive elements. The spline or serration must withstand repeated torque without excessive deformation or wear. The sintered iron-based material is designed to provide the required structural support for this function.
Because washing machines regularly change operating conditions, the part must remain reliable through repeated starts, stops, reversals, and load fluctuations. Stable material properties and controlled profiles help support consistent transmission behavior.
Household Appliance Production
Large-scale appliance production requires components that are economical, repeatable, and suitable for automated or semi-automated assembly. Powder metallurgy supports these requirements by producing near-net-shape parts with consistent dimensions and integrated features.
The process can also support product families. Different washing machine models may use components with similar basic designs but different diameters, thicknesses, or spline configurations. A manufacturer with suitable tooling and engineering capability can develop a range of customized variants while maintaining a common quality system.
Quality, Reliability, and Supply Considerations
Product reliability starts with a clearly defined specification. The drawing should identify dimensions, tolerances, material, surface treatment, appearance, inspection requirements, and any special functional tests. Clear requirements allow the supplier to create an appropriate process control plan.
Production reliability depends on stable raw materials, maintained tooling, controlled pressing conditions, consistent furnace operation, and effective inspection. Tool wear should be monitored because it can gradually affect profile dimensions. Furnace performance should also be controlled to maintain consistent sintering results.
Supply reliability requires more than manufacturing capacity. It also depends on communication, production planning, quality records, sample approval, packaging, and delivery coordination. A supplier with integrated engineering, production, and quality functions can respond more effectively when a project requires technical changes or volume adjustments.
Packaging should protect the blackened surface and prevent damage to the spline and serration profiles during transportation. Storage conditions should also be considered, particularly when parts will remain in inventory before assembly. Proper packaging and handling help preserve the finished condition of the component.
Economic and Environmental Benefits
Powder metallurgy can reduce material waste because the amount of powder placed into the die is closely related to the mass of the finished component. This is different from processes that begin with a larger block and remove excess material through turning, milling, broaching, or grinding.
Reduced machining can also decrease energy consumption associated with material removal and shorten the overall production route. The exact environmental benefit depends on the material, equipment, production volume, and process conditions, but efficient material utilization is a fundamental advantage of the technology.
Longer service life can provide an additional benefit. A durable clutch or transmission component may reduce the likelihood of premature replacement and help maintain appliance performance over a longer operating period. Reliability, material efficiency, and reduced secondary processing together make powder metallurgy an attractive manufacturing option for high-volume household appliances.
Technical Support for International Customers
International OEM and ODM customers may require assistance with metric dimensions, drawing interpretation, material selection, sampling procedures, inspection documentation, and production planning. Technical support should be available throughout the project rather than only after the purchase order is issued.
Free technical drawing support and sample testing can help customers determine whether the proposed component will fit their washing machine assembly. Engineering communication is especially important when the customer is changing from a machined or forged part to a powder metallurgy design.
The supplier can support prototype development, customized tooling, material evaluation, dimensional inspection, and mass production scaling. This enables customers to use one technical partner for multiple stages of product development and supply.
Q&A
What are these powder metallurgy structural components used for?
They are primarily used in washing machine clutch assemblies and transmission systems. Their inner spline or serration transfers torque to a mating shaft or component, while the outer serrated or geared profile can engage with a clutch or transmission mechanism.
Which materials are available?
Typical material systems include iron-based Fe-Cu-C and Fe-Ni-C powder metallurgy alloys. The exact formulation can be customized according to required strength, wear resistance, dimensional stability, operating conditions, and customer specifications.
How are the components manufactured?
The general process includes powder preparation, precision die compaction, high-temperature sintering, and blackening treatment. Inspection is conducted throughout the process and on the finished parts to verify dimensions, appearance, and required mechanical characteristics.
Why is powder metallurgy suitable for washing machine parts?
Powder metallurgy can produce near-net-shape components with complex internal and external profiles. It reduces material waste and secondary machining while providing repeatable dimensions, stable mechanical properties, and economical production for medium and high volumes.
What is the purpose of the black oxide treatment?
Blackening forms a dark oxide layer that improves surface appearance and supports corrosion resistance and anti-rust performance. It can also complement the wear and friction behavior of the sintered component in repeated mechanical service.
Can the spline and serration profiles be customized?
Yes. Inner and outer profiles, dimensions, tooth configurations, and other functional features can be developed according to customer drawings, samples, or assembly requirements. A design review is recommended before tooling begins.
Can the components be supplied in different sizes?
Yes. Small and large variants can be produced according to the washing machine model and transmission design. The final size range depends on the component geometry, required tolerances, production volume, and tooling feasibility.
What quality certifications support production?
The manufacturing organization operates under ISO 9001:2015 and IATF 16949:2016 quality management certifications. These systems support documented process control, inspection, traceability, corrective action, and continual improvement.
Can samples be tested before mass production?
Yes. Prototype samples and sample testing are available for OEM and ODM projects. Customers can use the samples to confirm assembly fit, spline or serration engagement, appearance, and initial performance before approving volume production.
What information should a customer provide for a quotation?
Useful information includes a drawing or sample, material preference, surface treatment requirement, annual or monthly quantity, critical tolerances, application conditions, packaging needs, and delivery destination. Additional assembly information can help engineers evaluate torque, fit, and wear requirements.
How does powder metallurgy compare with machined steel?
Machining can provide high accuracy but may require substantial material removal and several operations to create internal and external profiles. Powder metallurgy can form many features directly during compaction, reducing waste and production time. The best choice depends on the geometry, quantity, tolerance, and performance requirements.
Is blackening a replacement for lubrication?
No. Blackening provides surface protection and can support surface performance, but it does not replace lubrication where lubrication is required by the clutch or transmission design. The complete assembly should be evaluated with the specified lubricant and mating materials.
Conclusion
Powder metallurgy structural components offer a practical and technically capable solution for washing machine clutch and transmission systems. Their combination of iron-based alloy strength, near-net-shape manufacturing, complex profile formation, black oxide surface treatment, and dimensional stability makes them suitable for repeated torque transmission and mechanical engagement.
The manufacturing route of compaction, high-temperature sintering, and blackening reduces material waste and secondary machining while supporting consistent production. Internal splines, external serrations, and other functional features can be integrated directly into the component, helping improve assembly efficiency and reduce total manufacturing cost.
For OEM and ODM customers, the main advantage is the combination of product performance and development support. Customized materials, dimensions, spline configurations, surface treatments, samples, and production plans can be developed according to specific washing machine requirements. Experienced engineering personnel, modern production equipment, quality certifications, and an established manufacturing base provide a strong foundation for reliable long-term supply.
When selecting a supplier, customers should evaluate not only the individual component but also the complete production system behind it. Powder preparation, tooling design, compaction control, sintering stability, blackening quality, inspection capability, technical communication, and production scalability all contribute to the final result. A supplier with strength in each of these areas can deliver structural components that meet performance requirements while maintaining competitive and consistent manufacturing costs.
References
1. Powder Metallurgy Design Manual, principles of powder selection, compaction, sintering, and dimensional control.
2. ASM Handbook, Volume 7: Powder Metal Technologies and Applications.
3. ISO 9001:2015, Quality Management Systems — Requirements.
4. IATF 16949:2016, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
5. Standard engineering practices for the design and inspection of splined and serrated torque-transmission components.
6. Technical information supplied for iron-based powder metallurgy structural components used in washing machine clutch and transmission assemblies.
Product: Powder Metallurgy Structural Components for Washing Machines
Related products
-
-
Description: Custom powder metallurgy planetary gear with high precision, wear resistance for automotive, industrial machinery & home appliances. OEM/ODM supported.
See Details -
Product Description: High-precision powder metallurgy part (S14*7*10) made of iron material from Jiande Wefine, customized PM components with strict tolerance control.
See Details -
This copper-based powder metallurgy bushing is manufactured through an integrated process of compaction, sintering, sizing, and oil impregnation. It features excellent wear resistance and self-lubrica...
See Details -
This 4×11.5×5.2mm powder metallurgy gear is manufactured through a precise press-sinter-through hole-oil impregnation process, with strict control of press density (6.7–6.8g/cm³) and sintering tempera...
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Privacy Custom Self-lubricating Sintered Bushing Manufacturers
