E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Luo Qian — Product Sales Supervisor / Self-Lubricating Tin Bronze Flanged Bushings for Reliable Pump and Industrial Equipment Performance
Self-Lubricating Tin Bronze Flanged Bushings for Reliable Pump and Industrial Equipment Performance
 2026.11.07
 Luo Qian — Product Sales Supervisor
Content
- 1 What Is a Self-Lubricating Tin Bronze Flanged Bushing?
- 2 Why Tin Bronze Is Suitable for Flanged Bushings
- 3 How the Self-Lubricating Mechanism Works
- 4 Key Product Advantages
- 5 Powder Metallurgy Manufacturing Process
- 6 Technical Parameters and Design Considerations
- 7 Applications in Pump Systems
- 8 Applications Beyond Pumps
- 9 Comparison with Conventional Bushing Solutions
- 10 Manufacturing Strengths and Customization Capability
- 11 Quality Management and Customer Support
- 12 Installation Recommendations
- 13 Common Causes of Premature Failure
- 14 How to Select the Correct Bushing
- 15 Environmental and Cost Benefits
- 16 Q&A
- 16.1 What is the primary benefit of a self-lubricating flanged bushing?
- 16.2 Why is tin bronze used for this type of bushing?
- 16.3 Can the flange dimensions be customized?
- 16.4 Can the bushing operate completely without external lubrication?
- 16.5 Are these bushings suitable for water pumps?
- 16.6 What is the typical oil content?
- 16.7 What is the approximate operating temperature range?
- 16.8 How does the flange improve installation?
- 16.9 How should the bushing be installed?
- 16.10 Can the bushing be used in automotive components?
- 16.11 What quality certifications are available?
- 16.12 Can samples be produced before mass production?
- 16.13 What information should be provided for a quotation?
- 17 Conclusion
- 18 References
- 19 Product: Powder Metallurgy Self-lubricating Tin Bronze Flanged Bushing
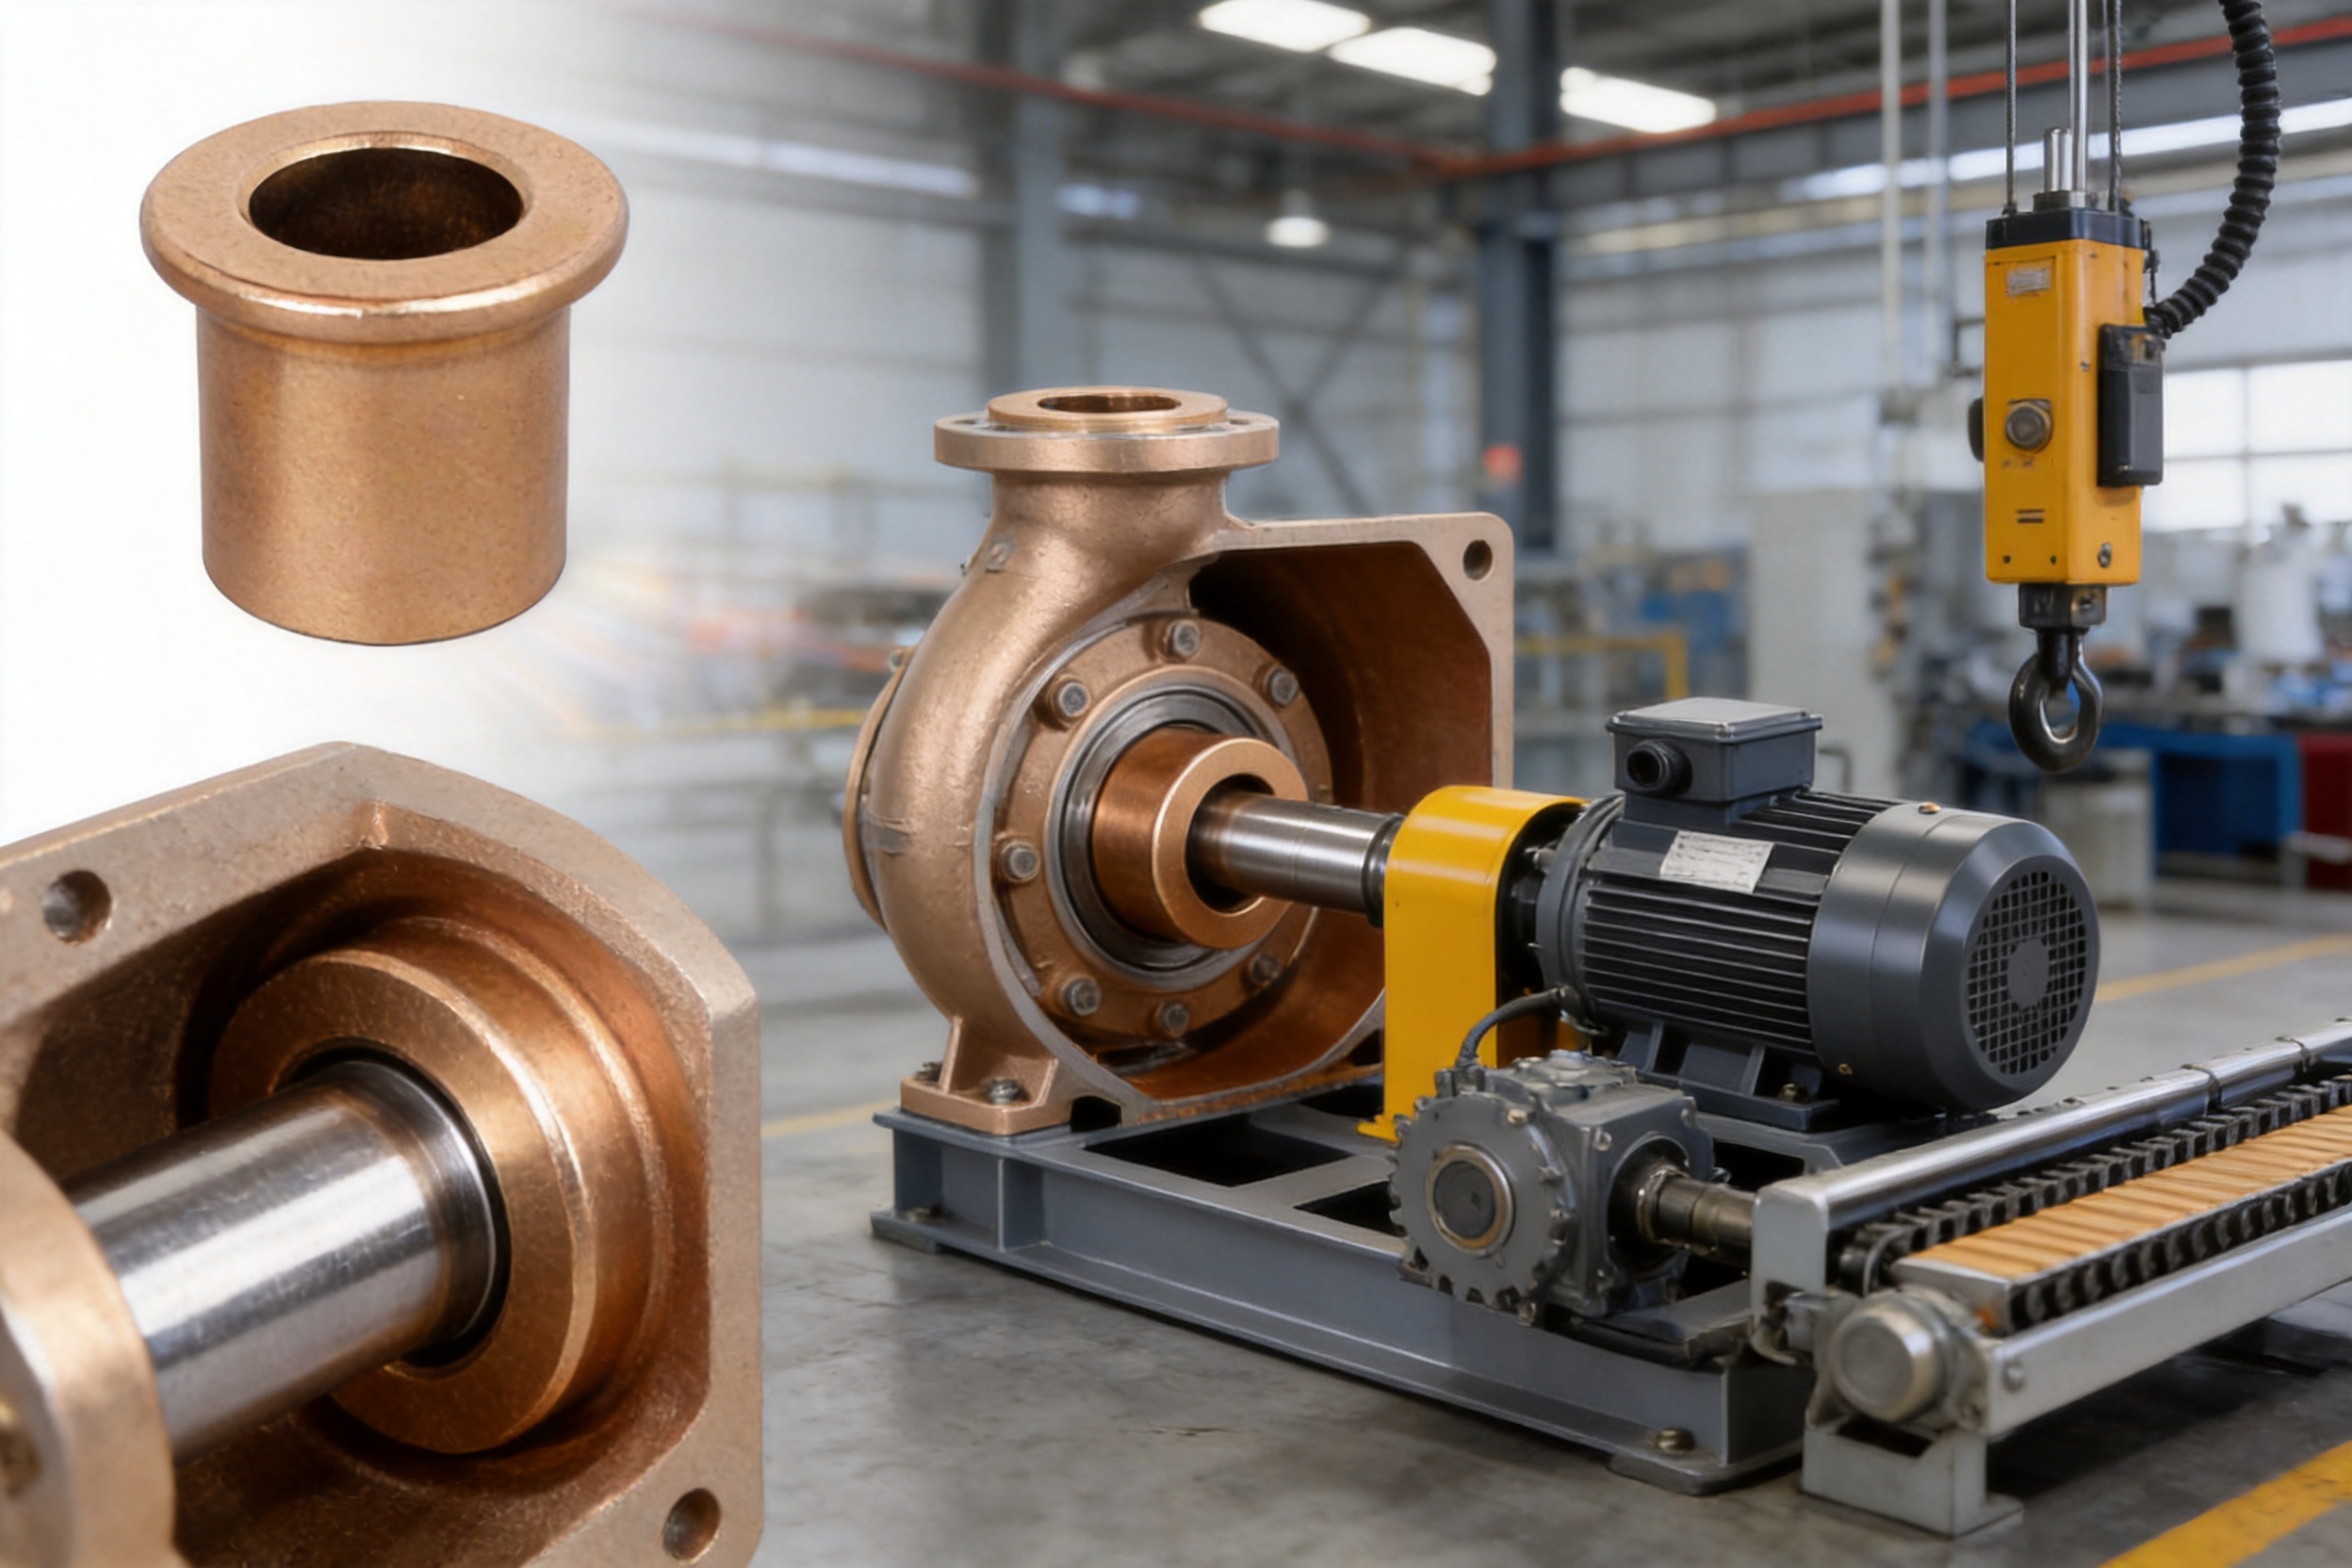
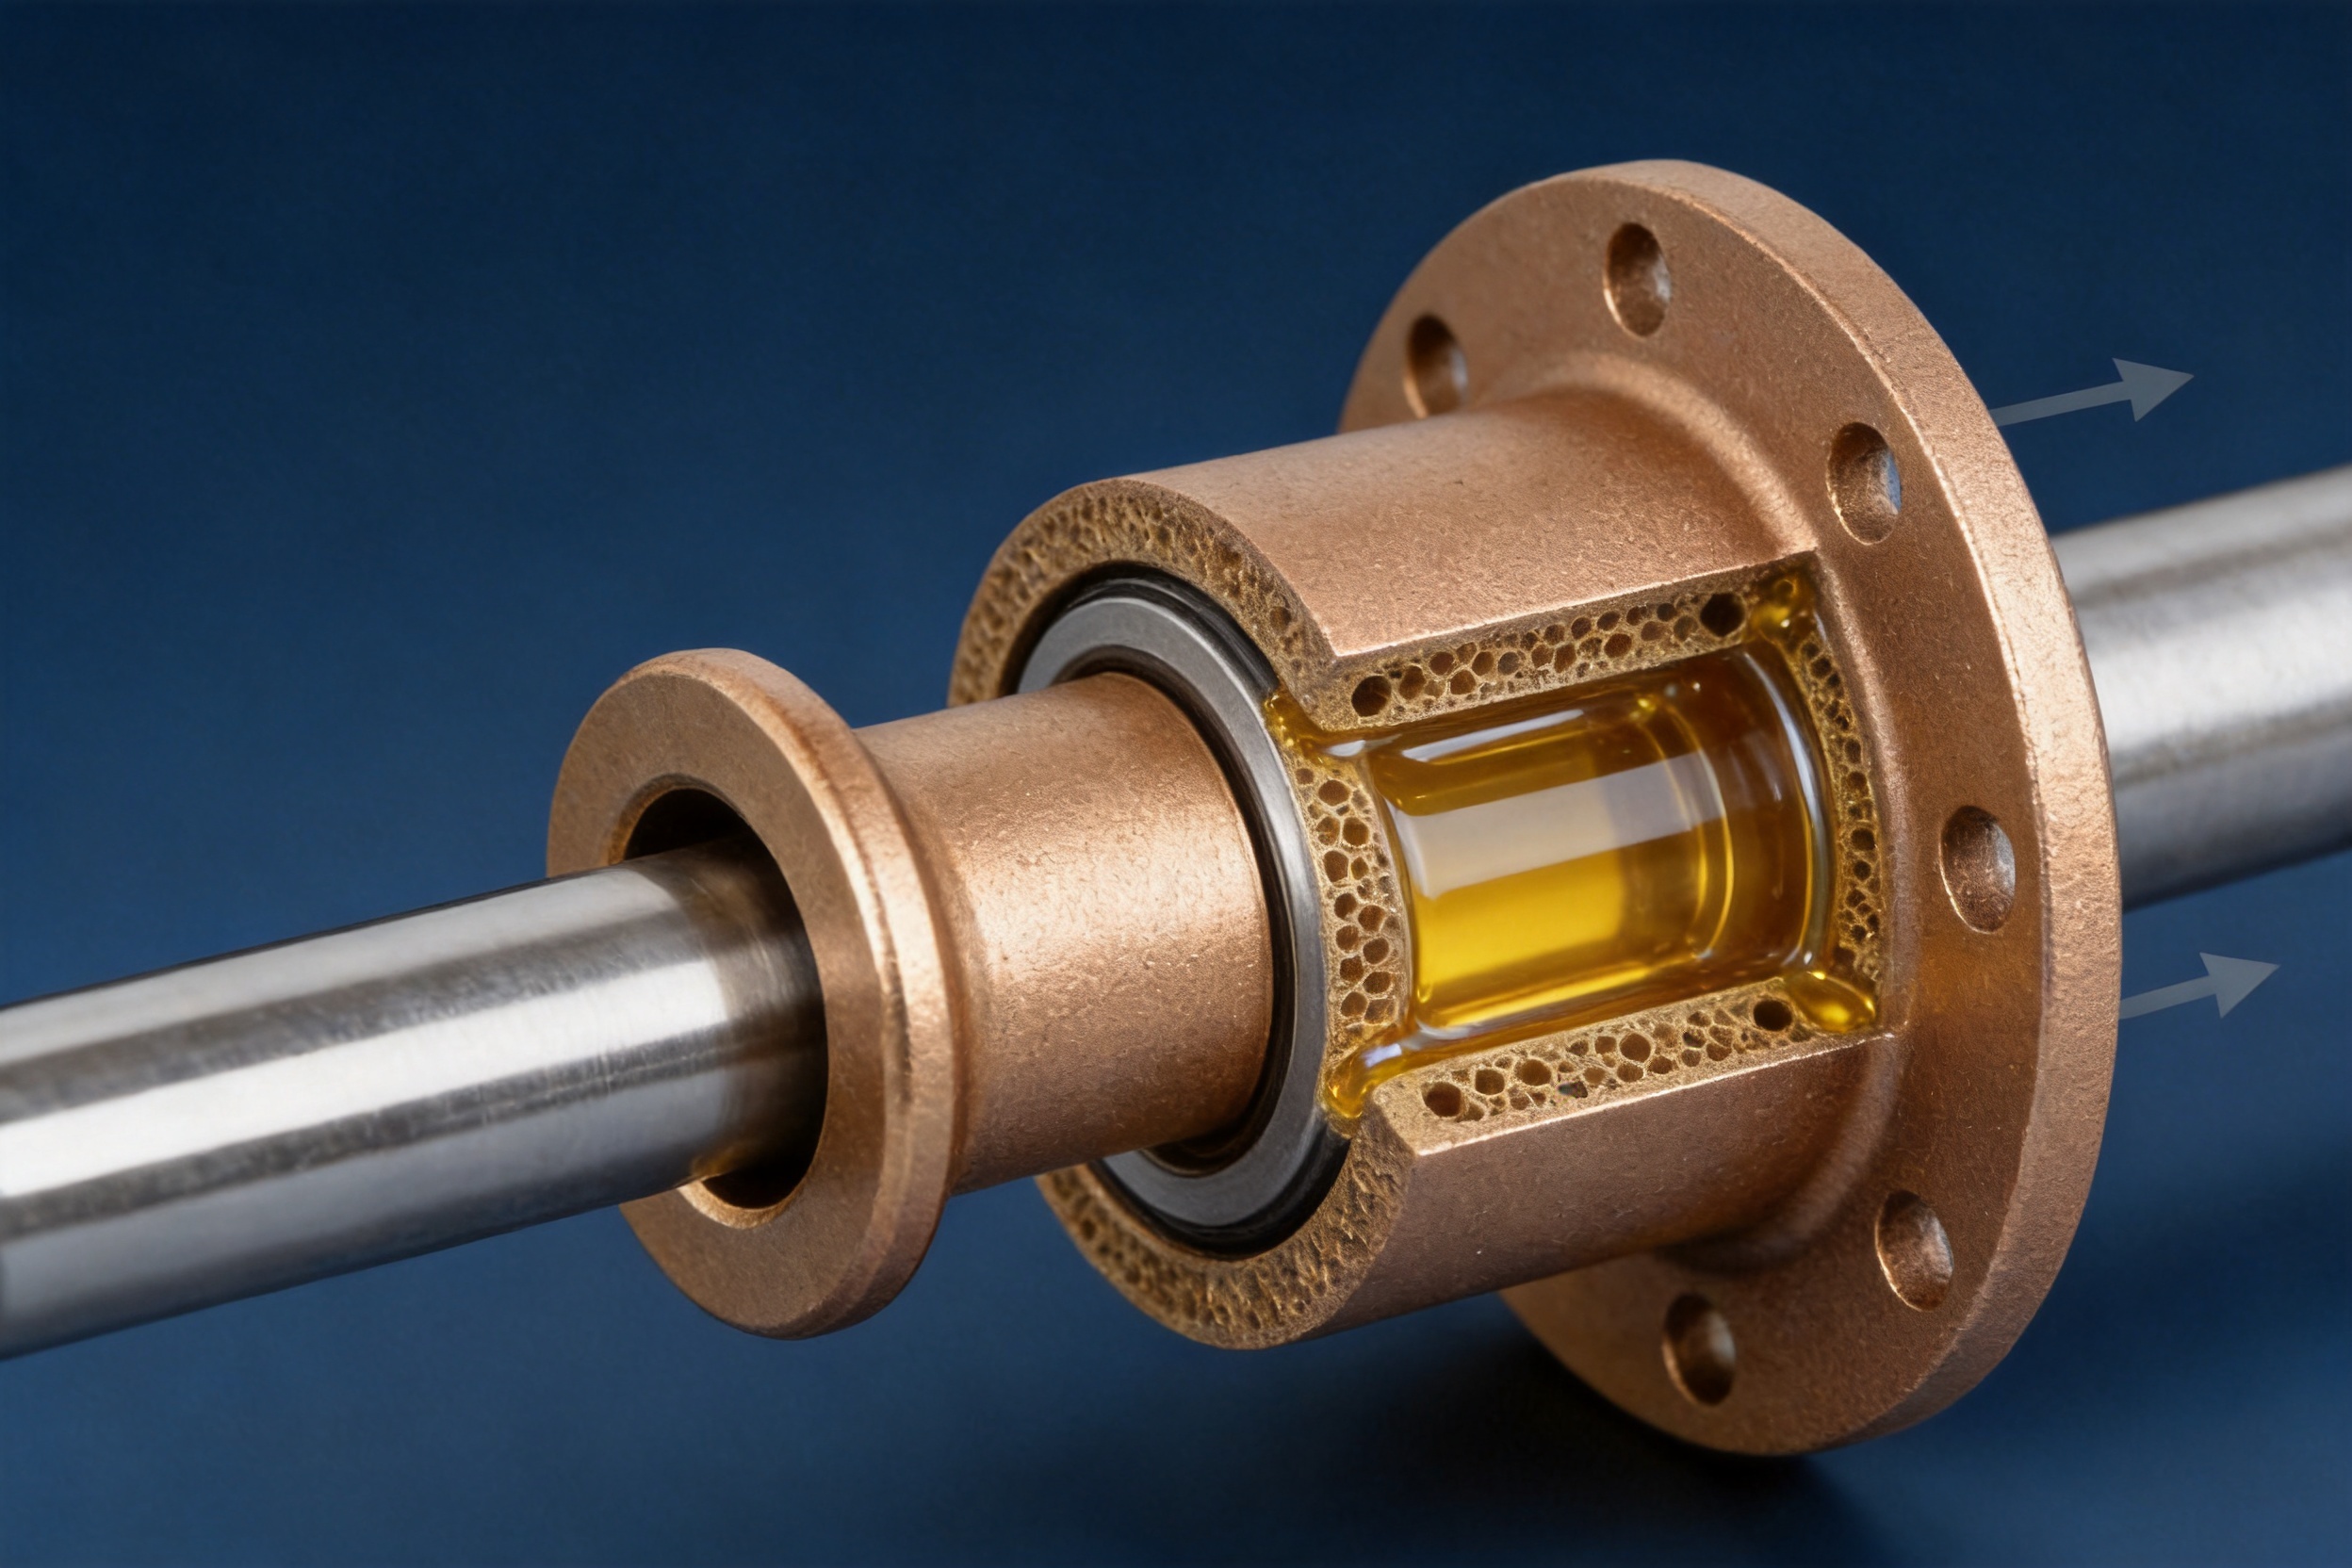
Self-lubricating tin bronze flanged bushings are engineered bearing components designed to support rotating or oscillating shafts while reducing friction, wear, maintenance requirements, and the risk of lubrication-related failure. Produced through powder metallurgy, these bushings contain a controlled network of internal pores that retain lubricating oil. During operation, the oil is released gradually to form a stable lubricating film between the bushing and shaft. When operation stops and the component cools, surplus oil can migrate back into the porous structure.
The integrated flange provides additional axial support and simplifies installation. Instead of requiring a separate thrust washer, spacer, or positioning component, the flange can help locate the bushing accurately within the housing. This construction is particularly useful in pumps, motors, reducers, hydraulic equipment, automotive mechanisms, construction machinery, conveyors, and precision industrial equipment.
For equipment manufacturers and maintenance professionals, the combination of porous tin bronze, oil impregnation, near-net-shape production, and one-piece flanged construction offers a practical alternative to conventional solid bronze bushings that depend on frequent external lubrication. The result is a compact bearing solution with stable dimensional accuracy, low maintenance demand, dependable wear resistance, and flexible customization options.
What Is a Self-Lubricating Tin Bronze Flanged Bushing?
A self-lubricating tin bronze flanged bushing is a cylindrical plain bearing with an integral flange at one end. The cylindrical body supports the shaft radially, while the flange provides axial positioning and may assist with axial load distribution. The component is made from sintered bronze powder that is compacted, sintered at high temperature, sized for dimensional accuracy, and impregnated with lubricating oil.
Unlike a rolling bearing, the bushing has no balls, rollers, cages, or complex raceway system. Its operation depends on sliding contact between the shaft and the bearing surface. The internal porosity of the sintered bronze is a key functional feature rather than a defect. These interconnected pores serve as small reservoirs for lubricant and allow the bushing to regulate oil at the working surface.
During shaft movement, frictional heat and capillary action encourage oil to reach the sliding interface. The oil forms a film that reduces direct metal-to-metal contact. When the temperature falls after operation, a portion of the lubricant returns to the pores. This reversible process allows the bushing to provide long-term lubrication without requiring a grease fitting or an external oil supply in many applications.
The product is commonly manufactured from tin bronze grades such as CuSn6 or CuSn8. These alloys combine good strength, toughness, wear resistance, and seizure resistance. The material is suitable for components that must withstand repeated movement, moderate impact, vibration, and continuous operation.
Why Tin Bronze Is Suitable for Flanged Bushings
Tin bronze is widely used for sliding bearing applications because it provides a balanced combination of mechanical and tribological properties. Copper supplies thermal conductivity and a stable metallic base, while tin improves strength, wear resistance, and resistance to friction-related damage.
One important advantage of tin bronze is its ability to operate reliably under conditions where a softer bearing material might deform excessively. The material can support shaft movement while maintaining a stable bearing surface. It also offers good resistance to seizure when the shaft and bushing experience increased load, speed, or temperature.
Tin bronze has useful heat-transfer characteristics. Frictional heat can be distributed through the bushing and transferred to the surrounding housing more effectively than with some lower-conductivity materials. This helps reduce localized hot spots and supports more stable operation in compact assemblies.
The material also provides good compatibility with common steel shafts. Proper shaft hardness, surface finish, clearance, and alignment remain important, but the bronze-steel combination is well established in pumps, gearboxes, motors, actuators, and general machinery.
Compared with many plastic bushings, sintered tin bronze can provide greater resistance to compression, creep, and elevated temperature. Compared with a conventional solid bronze bushing, the porous oil-impregnated structure offers a significant lubrication advantage. The selection of the correct material still depends on load, speed, temperature, environment, shaft material, and whether external lubrication is available.
How the Self-Lubricating Mechanism Works
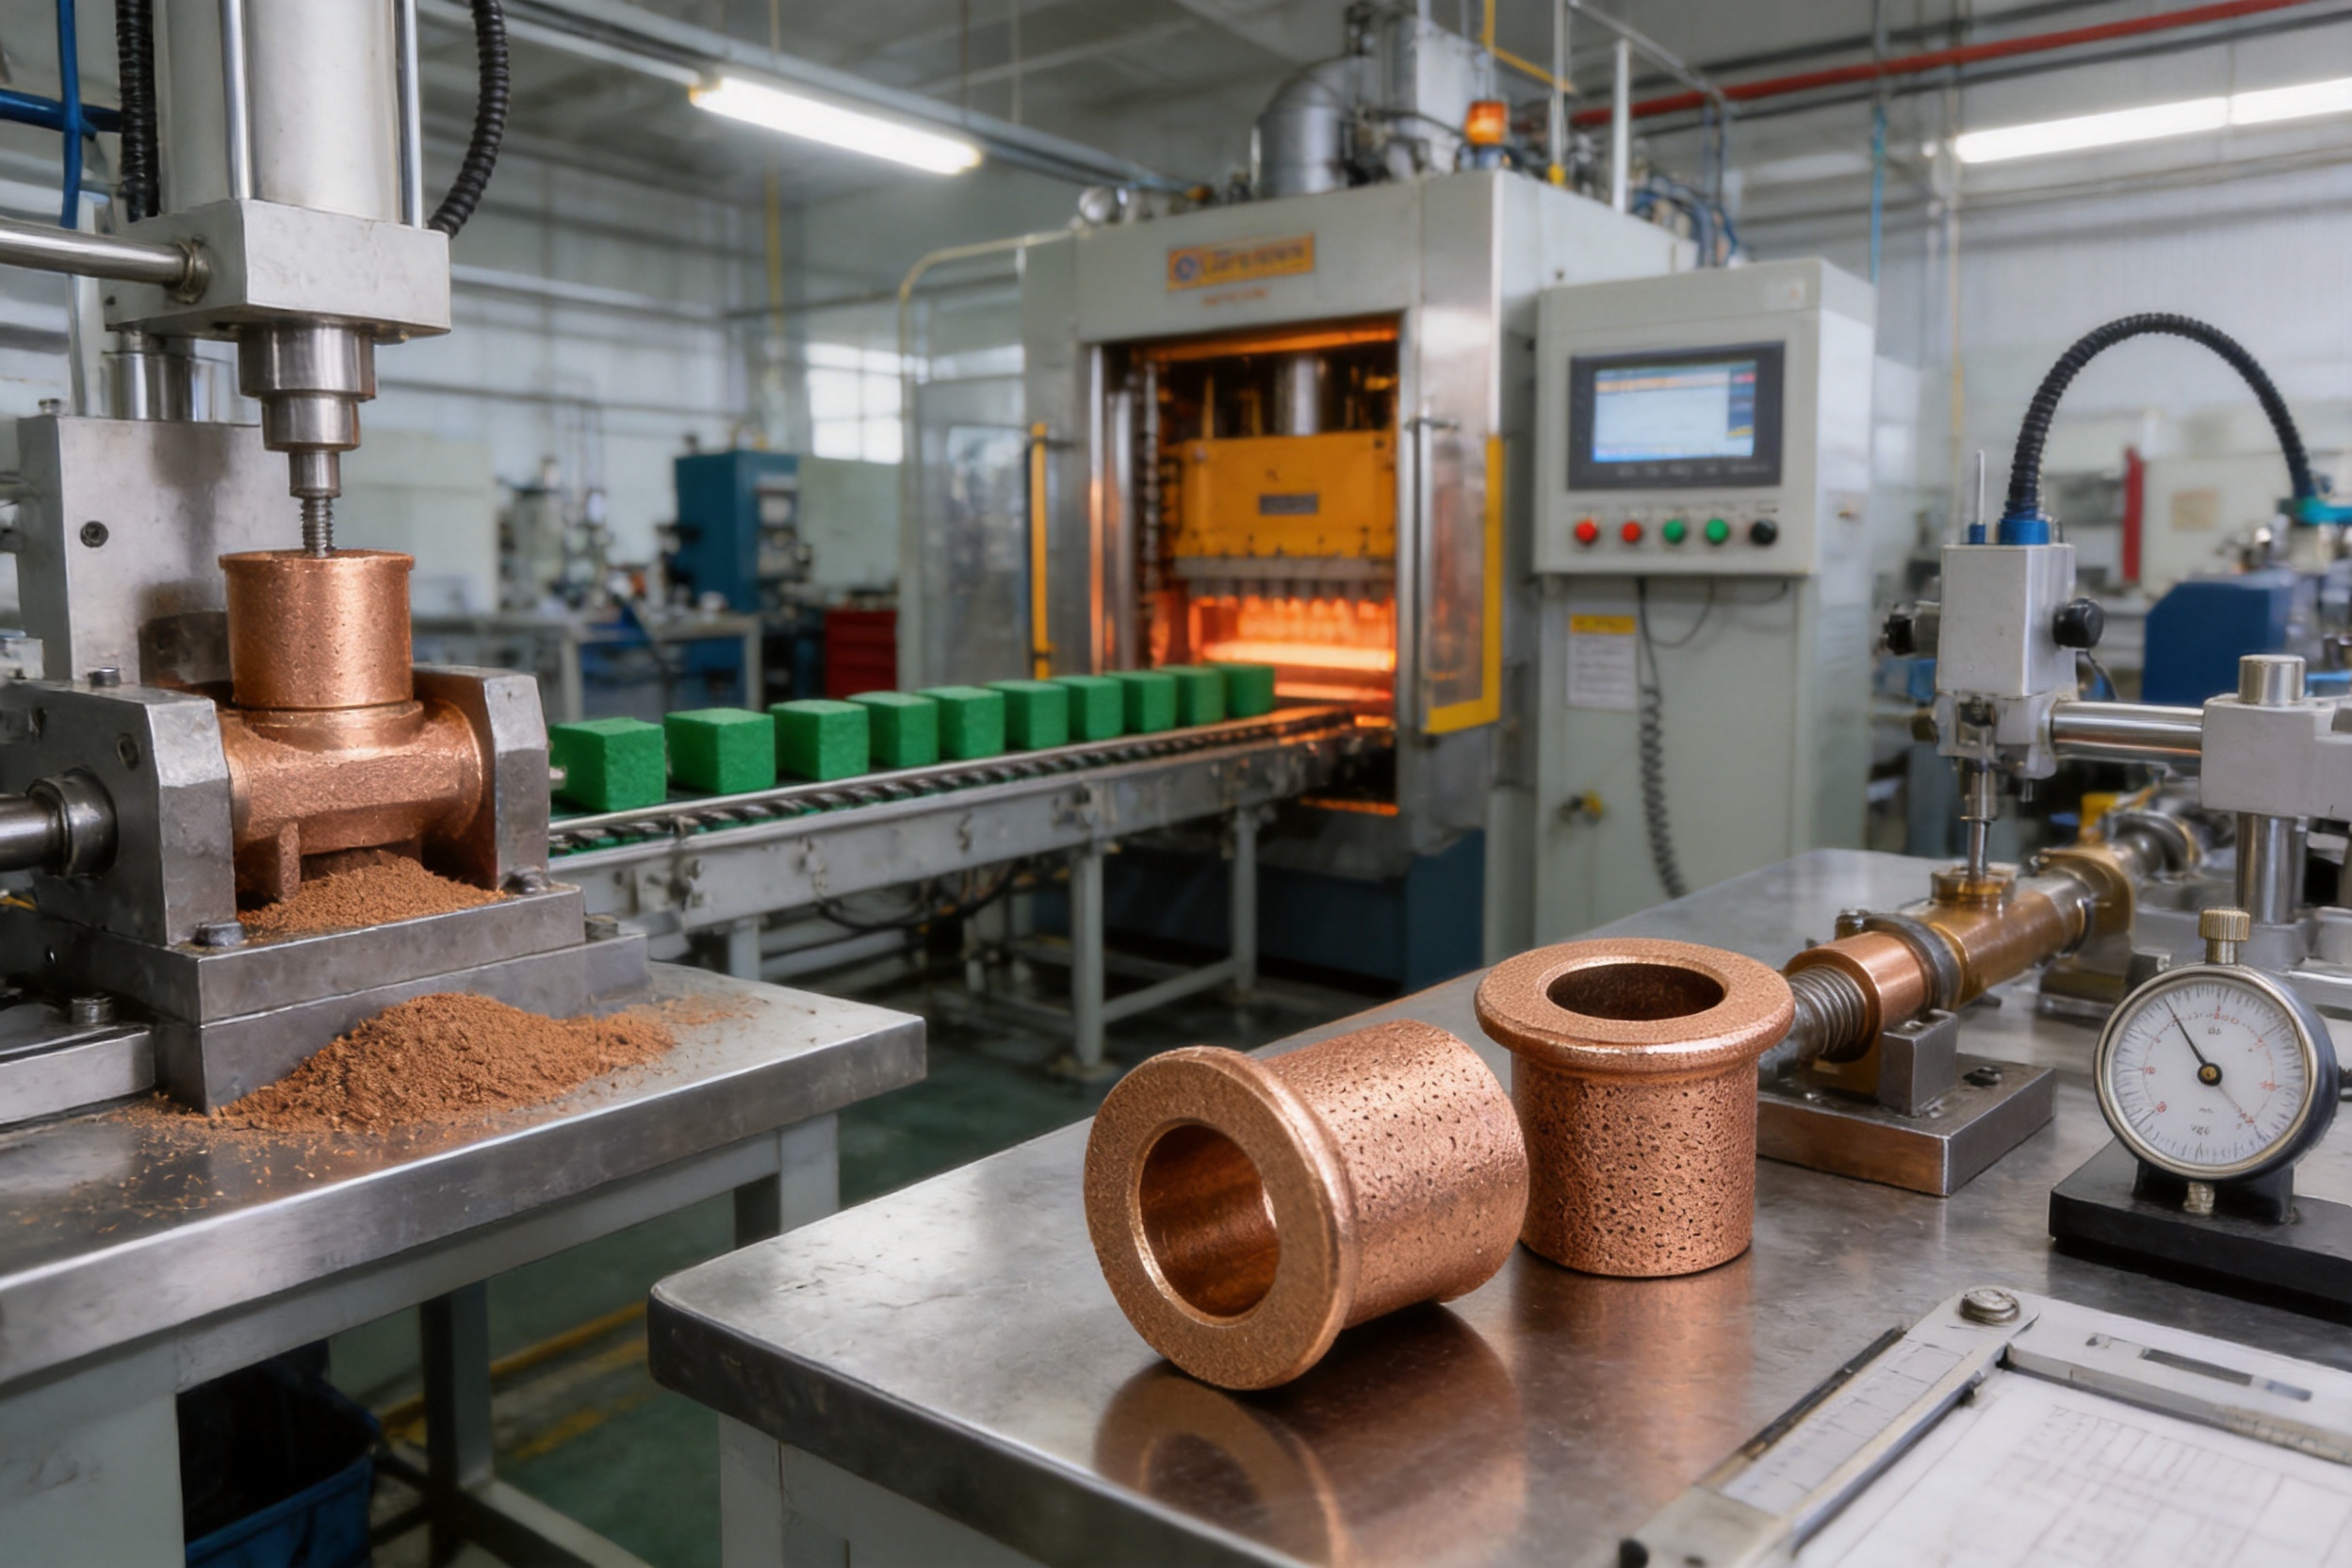
The self-lubricating function begins during powder metallurgy production. Metal powder is blended to achieve the required alloy composition and performance. The powder is then compacted in a precision die to create the approximate shape of the bushing. The compacted part contains interconnected voids that remain after sintering.
During high-temperature sintering, the powder particles bond together. The process gives the component its mechanical strength while preserving a controlled level of porosity. The size, distribution, and connectivity of the pores affect oil storage capacity, release behavior, density, strength, and dimensional stability.
After sintering, the bushing is sized to improve dimensional accuracy and control the bore geometry. It is then impregnated with lubricating oil under controlled conditions. The oil fills the internal pore network, with typical oil content reaching at least 18 percent depending on the design and material specification.
When the shaft rotates or oscillates, friction produces a small amount of heat at the interface. The oil within the pores becomes more mobile and gradually moves toward the bearing surface. A lubricating film develops between the shaft and bronze surface, reducing friction and wear.
When movement slows or stops, the temperature decreases. Excess oil can be drawn back into the pores through capillary action. This storage-and-release cycle allows the component to respond to operating conditions without a pump, grease gun, centralized lubrication system, or manually scheduled oil application.
The self-lubricating mechanism does not mean that the bushing is suitable for every environment without maintenance. Severe contamination, chemical attack, excessive load, improper clearance, shaft misalignment, or temperatures beyond the oil specification can reduce service life. However, in appropriately selected applications, internal oil impregnation substantially reduces lubrication-related maintenance and improves operating consistency.
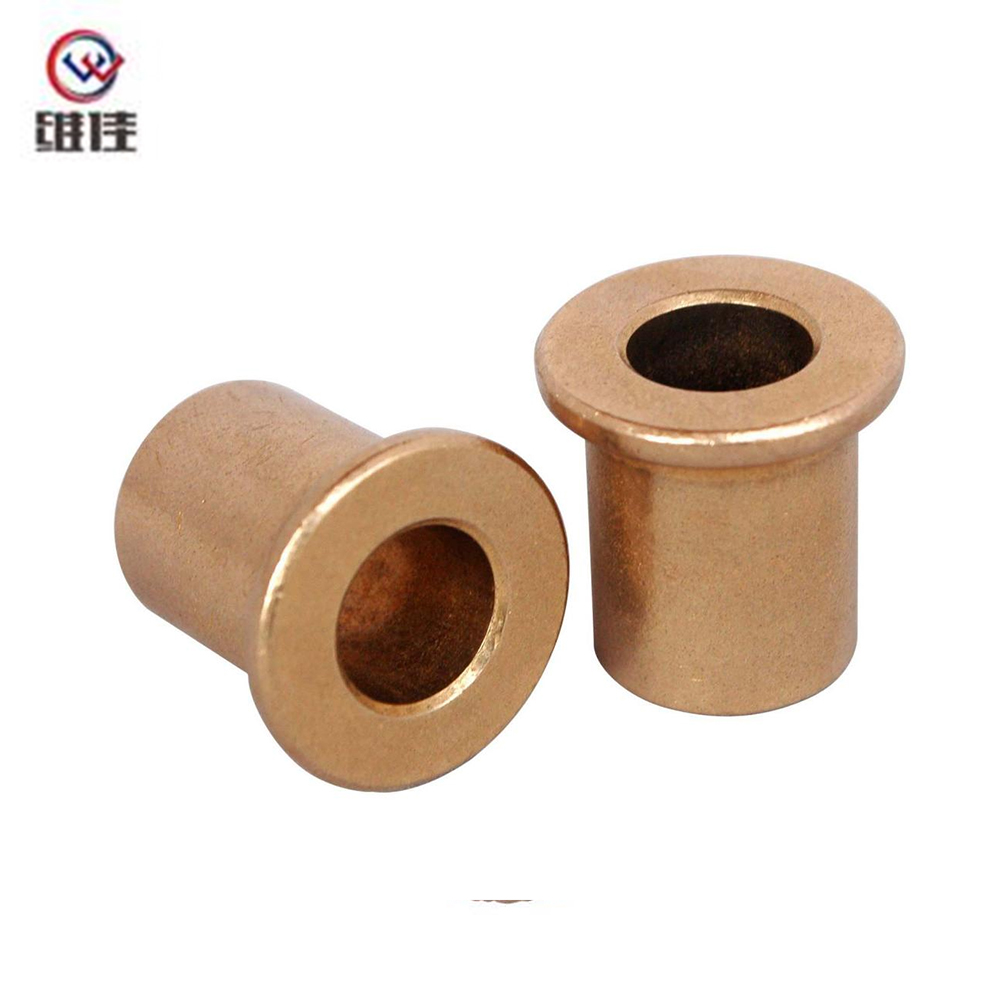
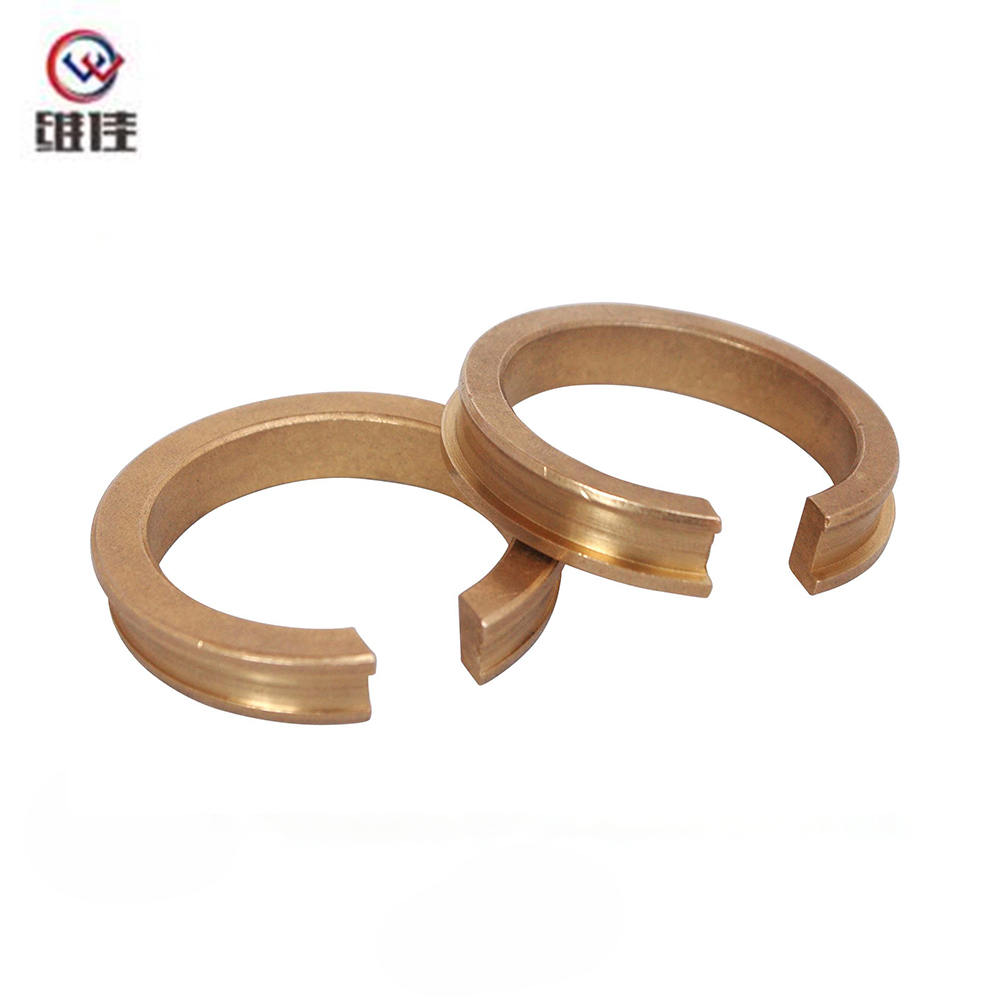
Powder Metallurgy Self-lubricating Tin Bronze Flanged Bushing
Key Product Advantages
Low Maintenance Operation
The most visible advantage of an oil-impregnated bushing is its ability to operate with little or no routine external lubrication. This is valuable in equipment where access is restricted, maintenance intervals are long, or manual lubrication would interrupt production.
Reducing lubrication tasks also reduces the possibility of human error. Incorrect lubricant quantity, missed lubrication intervals, incompatible grease, and contaminated application tools can all contribute to bearing failure. A properly impregnated bushing provides lubricant from within the component and reduces dependence on maintenance personnel for routine oil supply.
Reduced Friction and Wear
The lubricating film separates much of the sliding contact between the shaft and bearing surface. Lower direct contact can reduce the friction coefficient, operating temperature, vibration, and energy loss. It also protects the shaft from accelerated scoring and minimizes wear on the bushing itself.
Typical friction performance depends on shaft finish, speed, load, temperature, clearance, oil characteristics, and environmental conditions. Under suitable conditions, self-lubricating bronze bushings can achieve a friction coefficient in the approximate range of 0.05 to 0.15. Actual performance must be verified through application testing or engineering calculation.
Resistance to Wear and Seizure
Tin bronze provides a robust sliding surface for steel shafts. Its strength and toughness help it resist deformation under load, while the oil film reduces the probability of adhesive wear and seizure. The sintered structure also supports consistent lubrication across the working surface.
Seizure resistance is especially important in pumps, actuators, and mechanisms that may experience temporary overloads, start-stop cycles, or brief interruptions in ideal lubrication conditions. Although no bushing can compensate for severe overload or incorrect assembly, the combination of tin bronze and internal oil storage provides a useful safety margin.
Integrated Axial Positioning
The flange is formed as part of the bushing rather than added as a separate component. It can locate the bushing against a housing shoulder and prevent axial movement during operation. This simplifies assembly and can improve alignment between the shaft, housing, and adjacent components.
An integrated flange may also help distribute axial forces over a wider contact area. It can reduce the need for additional retaining rings, washers, or spacers, depending on the design. The flange dimensions can be customized to match the available housing geometry and required axial load.
Stable Performance During Continuous Operation
Industrial pumps, motors, fans, conveyors, and production machines may operate for thousands of hours each year. In these systems, a bearing that depends on frequent manual lubrication can become a maintenance bottleneck. An oil-impregnated bushing provides a more consistent lubrication source throughout repeated operating cycles.
Its performance is particularly useful in equipment where unexpected downtime is expensive. By reducing the likelihood of lubrication depletion caused by missed maintenance, the bushing can support greater equipment availability and more predictable service intervals.
Reduced Contamination Risk
External grease can attract dust, fibers, moisture, and abrasive particles. In dusty, wet, or dirty environments, these contaminants can become part of the sliding interface and accelerate wear. Since lubricant is stored inside the porous bronze, the self-lubricating design can reduce the amount of exposed grease on the outside of the assembly.
This advantage is relevant to agricultural machinery, construction equipment, material-handling systems, water-treatment installations, textile machinery, and industrial production lines. The housing should still be designed to protect the bearing from direct ingress of abrasive particles or corrosive chemicals.
Powder Metallurgy Manufacturing Process
Powder Selection and Material Blending
The manufacturing process begins with the selection of copper and tin-based powders that meet the required chemical composition, particle characteristics, cleanliness, and compressibility. Powder properties influence filling behavior, compact strength, sintered density, dimensional change, surface condition, and final mechanical performance.
Powders are blended under controlled conditions to achieve a uniform distribution of alloy constituents and processing additives. Uniform blending is important because local variation in composition can affect strength, porosity, wear behavior, and corrosion resistance.
Precision Powder Compaction
After blending, the powder is placed into a precision die and compacted under controlled pressure. The tooling creates the cylindrical bore, outside diameter, flange profile, and other design features required by the component drawing.
Powder compaction offers a major production advantage for bushings because it can create near-net-shape components with limited material waste. Compared with machining a bushing from a solid bronze bar, compaction can reduce the amount of material removed and shorten the number of machining operations.
Press settings, filling height, compaction pressure, tooling condition, and powder flow must be carefully controlled. Variations in these factors can lead to density gradients, cracks, dimensional instability, or inconsistent flange geometry.
High-Temperature Sintering
The compacted parts are heated in a controlled-atmosphere sintering furnace. At the appropriate temperature, the powder particles bond together through solid-state diffusion. Sintering develops the mechanical strength of the bushing while preserving the designed porous structure.
Temperature profile, atmosphere, heating rate, holding time, cooling rate, and furnace uniformity all influence the final product. A controlled atmosphere helps limit oxidation and supports repeatable material properties. The sintering schedule is developed according to the bronze composition, part geometry, density target, and required performance.
Sizing and Dimensional Calibration
After sintering, the bushing may require sizing to achieve the specified inner diameter, outer diameter, flange dimensions, and geometric tolerances. Sizing applies controlled force to improve dimensional consistency and surface condition without eliminating the useful porosity required for oil storage.
For suitable designs, dimensional accuracy can reach IT7 to IT8 levels after the appropriate forming and sizing operations. Final tolerances depend on component size, geometry, material, equipment capability, and drawing requirements.
Oil Impregnation
Oil impregnation fills the porous structure with a selected lubricant. The process may use vacuum, pressure, heating, or a combination of these methods to improve penetration. Controlled impregnation helps achieve consistent oil content throughout the production batch.
Typical oil content is at least 18 percent for the specified bronze bushing range, although the final value depends on density, porosity, oil type, and technical requirements. Oil selection should consider operating temperature, speed, load, chemical exposure, and compatibility with the surrounding system.
Optional Surface Treatments
Natural sintered bronze can be supplied when the application and environment permit. Phosphating or tin plating may be selected to improve corrosion resistance, surface behavior, appearance, or compatibility with the assembly environment.
Surface treatment must be selected carefully because excessive coating thickness or inappropriate processing can affect the bore, flange fit, oil release, or dimensional tolerances. Critical functional surfaces should be controlled through inspection after treatment.
Inspection and Quality Control
Quality control can include chemical composition verification, density testing, oil-content measurement, dimensional inspection, visual examination, hardness testing, porosity evaluation, and performance testing. Inspection frequency may be adjusted according to part criticality, production volume, customer standards, and certification requirements.
Batch inspection reports can provide traceability for material, dimensions, and manufacturing results. This is valuable for pump manufacturers and industrial customers that require consistent incoming quality and documented process control.
Technical Parameters and Design Considerations
The following values represent typical reference capabilities. Final specifications should be confirmed against the product drawing, operating conditions, and customer quality requirements.
| Parameter | Typical Reference Value |
| Material | Tin bronze, including CuSn6 or CuSn8 options |
| Oil content | 18 percent or higher, depending on design |
| Density | Approximately 6.2–6.8 g/cm³ |
| Inner diameter range | Approximately 3–100 mm |
| Outer diameter range | Approximately 6–120 mm |
| Length range | Approximately 5–100 mm |
| Flange diameter | Typically 2–10 mm larger than the outer diameter |
| Operating temperature | Approximately -40°C to +220°C, subject to lubricant and application conditions |
| Ultimate PV value | Approximately 2.5 MPa·m/s without additional oil lubrication |
| Dimensional accuracy | Up to IT7–IT8 for suitable designs and processes |
| Surface treatment | Natural finish, phosphating, or tin plating |
Load and Speed
The product must be selected according to both load and sliding speed. A bushing may support a high load at low speed or a lower load at high speed, but the combination of pressure and velocity determines the heat generated at the sliding interface. The PV value is a useful preliminary indicator of operating severity.
The ultimate PV value should not automatically be treated as a continuous design target. A suitable safety factor is normally required, particularly for start-stop operation, impact loading, poor alignment, elevated temperature, or contaminated environments. Engineers should evaluate dynamic load, static load, oscillation angle, duty cycle, and peak conditions.
Clearance and Shaft Fit
Correct operating clearance is essential. Excessive clearance may cause vibration, uneven pressure distribution, noise, and accelerated wear. Insufficient clearance may restrict oil movement, increase friction, and cause seizure when the shaft or housing expands thermally.
The recommended clearance depends on shaft diameter, temperature, speed, load, shaft material, surface finish, and housing conditions. The shaft should be free from burrs and sharp edges. A lead-in chamfer can reduce damage during assembly.
Shaft Surface Condition
The mating shaft should have a suitable hardness and surface finish. A rough shaft can abrade the bronze surface and disrupt the oil film, while an excessively soft shaft may develop grooves or transfer material into the bushing. The shaft should also be clean and free from rust, scale, machining chips, and abrasive particles.
Housing Design
The housing bore should be accurately machined and aligned with the shaft axis. The housing material must provide sufficient support to prevent the bushing from rotating or deforming under load. An interference fit may be required for the cylindrical body, but the fit must be controlled so that it does not reduce the internal clearance excessively.
The flange seating surface should be flat and free of burrs. If the flange is used to support axial load, the contact area and housing shoulder should be designed to prevent localized stress concentration.
Temperature and Lubricant Compatibility
The stated temperature range is a reference value and depends on the impregnated oil, shaft speed, load, heat dissipation, and surrounding components. Continuous operation near the upper temperature limit should be validated carefully.
Chemicals, cleaning agents, water, steam, and process fluids may affect the lubricant or bronze alloy. Where the bushing is exposed to aggressive chemicals or direct fluid immersion, material compatibility and sealing should be reviewed before production approval.
Applications in Pump Systems
Centrifugal Pumps
Centrifugal pumps often use bushings to support shafts, guide rotating assemblies, or maintain alignment between internal components. A flanged bushing can provide radial support while its flange establishes an axial reference point within the pump structure.
Self-lubricating operation can be useful where the pump is installed in a compact housing or where frequent disassembly is undesirable. The final selection must consider shaft speed, fluid temperature, pressure, possible fluid ingress, and whether the bushing operates in a dry, partially lubricated, or immersed condition.
Water Circulation Pumps
Water circulation equipment may operate continuously in industrial buildings, cooling systems, process lines, and municipal installations. Reduced maintenance is valuable because these pumps may be distributed throughout a facility or installed in locations that are difficult to access.
Where water can reach the bearing, the design should consider corrosion, lubricant washout, sealing, and the compatibility of the bushing with the actual fluid. A standard oil-impregnated bushing should not be assumed to be suitable for permanent immersion without application-specific verification.
Chemical Transfer Pumps
Chemical processing equipment requires careful evaluation of alloy and lubricant compatibility. Tin bronze can provide useful mechanical performance, but the chemical composition, concentration, temperature, and exposure duration of the process fluid must be reviewed. Protective seals or alternative materials may be needed in aggressive environments.
Agricultural Irrigation Pumps
Agricultural pumping systems can be exposed to dust, humidity, seasonal temperature changes, vibration, and irregular maintenance. A self-lubricating flanged bushing can reduce the effect of missed lubrication intervals and help maintain reliable shaft support during seasonal operation.
Industrial Cooling and Circulation Pumps
Cooling systems often run for extended periods and are closely connected to the operating continuity of production equipment. Lower friction and reduced maintenance can help support stable operation and reduce the need for frequent planned shutdowns.
Marine and Auxiliary Pump Systems
Marine equipment may have limited access to service points and may be exposed to moisture, vibration, and salt-containing atmospheres. Proper housing protection and corrosion control remain essential. A suitable surface treatment, environmental seal, or specialized material may be considered based on the installation conditions.
Applications Beyond Pumps
The same bushing design can be used in many systems that require compact, low-maintenance sliding support. Automotive applications include steering mechanisms, brake pedal assemblies, seat adjustment systems, hinge points, and actuator linkages.
Construction machinery may use flanged bushings in excavator and loader mechanisms, hydraulic valve groups, control linkages, and other moving joints. In these applications, the bushing must be selected for impact loads, oscillating motion, dirt exposure, and intermittent operation.
Textile machinery and printing equipment can benefit from low-friction components that operate quietly and require limited service intervention. Office equipment, small motors, gear reducers, conveyors, and general transmission systems may also use oil-impregnated bushings for rotating or oscillating shafts.
Because the product can be customized in inner diameter, outer diameter, length, flange size, material grade, and surface treatment, it can be adapted to both standard assemblies and specialized OEM designs.
Comparison with Conventional Bushing Solutions
Conventional solid bronze bushings are strong and versatile, but they generally rely on external oil or grease. If the lubricant is not replenished at the correct interval, friction and wear may increase. External lubrication systems can also add fittings, channels, seals, labor, and maintenance procedures.
Plastic bushings can provide low friction and corrosion resistance in selected applications, but some plastics may experience creep, dimensional changes, or reduced load capacity at elevated temperatures. Their performance can also vary with moisture absorption and thermal expansion.
Rolling bearings can provide low friction at higher speeds, but they include more parts, require controlled installation, and may be more sensitive to contamination or shock loading. They can also require seals, grease, or oil circulation systems.
The self-lubricating tin bronze flanged bushing offers a practical balance for applications that require a simple, compact, economical, and low-maintenance sliding bearing. It is especially attractive when the operating speed and load are within the capability of a plain bearing and when a flange can simplify axial positioning.
| Performance Factor | Self-Lubricating Flanged Bronze Bushing | Conventional Solid Bronze Bushing | Typical Plastic Bushing |
| Lubrication method | Internal oil impregnation | External grease or oil | Material-dependent, often dry running |
| Routine lubrication demand | Very low in suitable conditions | Regular lubrication commonly required | Usually low, but application dependent |
| Load stability | Good for designed PV range | Good with adequate lubrication | Varies with polymer and temperature |
| Temperature capability | Approximately -40°C to +220°C, subject to oil | Depends on alloy and lubricant | Often more limited at elevated temperature |
| Axial positioning | Integrated flange | Requires flanged design or additional parts | Design dependent |
| Contamination exposure | Reduced external lubricant exposure | External lubricant may attract contaminants | Material may be sensitive to particles |
| Manufacturing efficiency | Near-net-shape powder metallurgy | More machining may be required | Molding or machining dependent |
Manufacturing Strengths and Customization Capability
Jiande Welfine Technology Co., Ltd. was established in 2001 and focuses on powder metallurgy sintering, self-lubricating bushings, and related precision components. Its production and engineering capabilities are designed to support both standard parts and custom OEM or ODM requirements.
The company operates a modern production base covering approximately 13,039 square meters and employs more than 150 skilled personnel. The facility includes high-efficiency presses, high-temperature sintering furnaces, precision forming equipment, and inspection resources. This combination supports consistent production from powder preparation through final dimensional control.
More than two decades of experience in powder metallurgy provide practical knowledge in tooling design, powder compaction, sintering control, sizing, oil impregnation, and production troubleshooting. Customers can provide drawings, samples, performance requirements, or assembly information for technical evaluation.
Customization may include inner diameter, outer diameter, length, flange diameter, flange thickness, chamfer dimensions, oil type, bronze grade, density, surface treatment, packaging, and inspection documentation. Small-batch trial production can be supported before full-scale manufacturing, allowing customers to verify fit and performance in the intended assembly.
Near-net-shape production can reduce machining allowance and material waste. For suitable designs, this may reduce total component cost by more than 30 percent compared with traditionally machined copper or bronze bushings. Actual savings depend on geometry, annual volume, tolerance requirements, tooling, secondary operations, and inspection specifications.
Standard parts may be available from inventory, while custom products can often be scheduled for delivery within approximately 7–15 days after drawing confirmation and production approval. Delivery time depends on tooling requirements, order quantity, material availability, surface treatment, and quality documentation.
Quality Management and Customer Support
Reliable bushing performance depends on repeatable processes rather than material selection alone. The company applies process control across powder preparation, compaction, sintering, sizing, oil impregnation, surface treatment, inspection, and packaging.
Jiande Welfine Technology Co., Ltd. maintains ISO 9001:2015 and IATF 16949:2016 certifications. These systems support documented procedures, traceability, corrective action, process monitoring, and continuous improvement. The IATF-based approach is particularly relevant to customers supplying automotive or automotive-related assemblies that require disciplined quality management.
Material and dimensional inspection reports can be supplied for production batches according to customer requirements. These reports may include dimensions, density, oil content, material information, and other agreed characteristics.
Technical support is available during product selection, drawing review, prototype development, installation, and maintenance planning. Early communication is encouraged because small changes in flange geometry, bore tolerance, oil specification, or housing fit can significantly affect the final performance of the assembly.
Packaging is designed to protect the bushings from moisture, oxidation, contamination, and transit damage. Independent moisture-resistant packaging can help preserve the surface condition and lubricant quality before installation.
A 12-month warranty is offered for non-human-induced product damage under the agreed conditions. Warranty evaluation should consider installation method, operating load, lubrication conditions, shaft condition, environmental exposure, and application history.
Installation Recommendations
Inspect Before Assembly
Before installation, inspect the bushing for dents, cracks, corrosion, contamination, damaged flange edges, or blocked bore surfaces. Confirm the part number, dimensions, material, and orientation against the assembly drawing.
Prepare the Housing and Shaft
Clean the housing bore and shaft thoroughly. Remove chips, dust, rust, burrs, and remnants of old lubricant. Check that the housing is round and aligned, and verify that the shaft diameter and surface finish meet the design requirements.
Use Suitable Pressing Equipment
Press the bushing into the housing using a suitable mandrel that applies force evenly to the correct surface. Do not hammer directly on the flange or use a tool that can deform the bore. The pressing force should be aligned with the bushing axis.
Protect the Flange
Ensure that the flange seats against a clean, flat shoulder without distortion. The flange should not be used to correct a misaligned housing or force the bushing into an incorrectly machined seat.
Verify Bore Condition After Pressing
After installation, measure the bore or verify shaft fit according to the assembly specification. Housing interference can reduce the bushing bore, so the final installed condition is more important than the free-state dimension alone.
Control Initial Operation
Where possible, operate the equipment initially at reduced speed and load. Listen for abnormal noise, check vibration and temperature, and confirm that the shaft rotates freely. Any rapid temperature rise, seizure, scoring, or unusual vibration should be investigated immediately.
Common Causes of Premature Failure
Incorrect clearance is one of the most common causes of bushing failure. Too little clearance can create excessive friction and heat, while too much clearance can lead to impact, vibration, edge loading, and uneven wear.
Misalignment causes the shaft to load one side of the bushing. This can result in localized wear, overheating, flange stress, and shortened service life. The housing, shaft, and adjacent components should be aligned during assembly.
Contamination can scratch the bearing surface and damage the oil film. Abrasive particles should be prevented from entering the assembly through appropriate sealing, shielding, or housing design.
Overloading or exceeding the recommended PV value can generate more heat than the bushing can dissipate. Impact loads and repeated starts may be more severe than a simple average-load calculation suggests.
Incorrect installation can deform the flange or reduce the bore. Direct hammering, use of an undersized mandrel, pressing against the wrong surface, or installing the part into a rough housing can cause immediate damage.
Improper storage can expose the bushing to moisture, dust, and oxidation. Components should remain in their protective packaging until they are ready for installation and should be stored in a clean, dry environment.
How to Select the Correct Bushing
Begin with the shaft diameter, housing dimensions, available axial space, and required flange profile. Then define the movement type: continuous rotation, intermittent rotation, oscillation, reciprocation, or start-stop movement.
Record the radial load, axial load, peak load, shaft speed, duty cycle, operating temperature, and expected service life. Include transient conditions such as startup, emergency stops, overloads, vibration, and shock.
Evaluate the environment, including dust, water, humidity, chemicals, process fluids, salt spray, cleaning agents, and outdoor exposure. Determine whether a natural finish, phosphating, tin plating, additional sealing, or another material should be considered.
Confirm the shaft material, hardness, roughness, roundness, and alignment. Check whether the shaft is hardened, plated, ground, or coated. The mating surface is a critical part of the bearing system and should be included in the engineering review.
Finally, select the required documentation and inspection level. For automotive, pump, or safety-related applications, customers may require material certificates, dimensional reports, capability studies, batch traceability, or performance testing.
Environmental and Cost Benefits
Powder metallurgy can reduce material waste because the component is formed close to its final shape. Less machining produces less scrap and can reduce energy consumption associated with removing large amounts of material from a solid bronze blank.
Internal lubrication can also reduce the consumption of grease and oil during service. Fewer lubrication operations mean less lubricant handling, fewer replacement materials, and reduced maintenance labor.
Longer service life helps reduce the frequency of replacement and the associated cost of downtime, disassembly, transportation, and disposal. These benefits are particularly important in large production lines and equipment installed in remote or difficult-to-access locations.
Environmental performance depends on the full product life cycle, including powder production, sintering energy, lubricant selection, packaging, service conditions, and end-of-life recycling. Tin bronze remains a recoverable copper-based material, and responsible recycling can help recover valuable metal resources.
Q&A
What is the primary benefit of a self-lubricating flanged bushing?
The primary benefit is the ability to provide internal lubrication during operation without relying on frequent external grease or oil application. The porous bronze stores lubricant and releases it to the sliding surface as operating conditions change. The flange additionally supports axial positioning and can simplify assembly.
Why is tin bronze used for this type of bushing?
Tin bronze offers good strength, toughness, wear resistance, thermal conductivity, and resistance to seizure. It is also compatible with many steel shafts when the shaft finish, clearance, load, and speed are properly selected.
Can the flange dimensions be customized?
Yes. Inner diameter, outer diameter, length, flange diameter, flange thickness, chamfers, material grade, oil type, and surface treatment can be customized according to drawings, samples, and application requirements.
Can the bushing operate completely without external lubrication?
In suitable applications, the oil-impregnated structure can support operation without routine external lubrication. However, the result depends on load, speed, temperature, environment, shaft condition, and duty cycle. Severe or unusual conditions should be reviewed by an engineer before approval.
Are these bushings suitable for water pumps?
They can be suitable for selected water pump applications, but direct water exposure, immersion, fluid chemistry, temperature, and sealing must be evaluated. Standard oil-impregnated bushings should not be used for permanent immersion without application-specific confirmation.
What is the typical oil content?
The reference oil content is at least 18 percent for the described product range. The actual value depends on bronze density, porosity, lubricant type, part geometry, and the agreed technical specification.
What is the approximate operating temperature range?
The reference range is approximately -40°C to +220°C. The actual allowable temperature depends on the oil, speed, load, heat dissipation, surrounding materials, and duration of operation.
How does the flange improve installation?
The integral flange can locate the bushing against a housing shoulder and help prevent axial movement. It can reduce the need for separate spacers or retaining components and can improve assembly consistency.
How should the bushing be installed?
The housing and shaft should be clean, accurately machined, aligned, and free from burrs. The bushing should be pressed into place using an aligned mandrel that distributes force evenly. Direct hammering on the flange or bore should be avoided.
Can the bushing be used in automotive components?
Yes. Potential automotive applications include steering systems, brake pedal mechanisms, seat adjustment systems, actuator linkages, and other moving assemblies. The final product must meet the required automotive drawing, validation, durability, and quality standards.
What quality certifications are available?
The manufacturer maintains ISO 9001:2015 and IATF 16949:2016 certifications. Batch inspection reports and other quality documentation can be arranged according to customer requirements.
Can samples be produced before mass production?
Yes. Custom development can begin from a drawing, sample, or application specification. Small-batch trial production allows customers to confirm fit, installation, friction behavior, wear performance, and compatibility before approving larger quantities.
What information should be provided for a quotation?
Useful information includes the drawing or sample, inner and outer diameters, length, flange dimensions, material preference, quantity, shaft material, load, speed, temperature, environment, lubrication conditions, surface treatment, inspection requirements, and expected delivery schedule.
Conclusion
Self-lubricating tin bronze flanged bushings provide a dependable and economical bearing solution for pumps, motors, automotive mechanisms, construction machinery, precision equipment, and general industrial systems. Their performance is based on the combined advantages of tin bronze, controlled powder metallurgy porosity, internal oil impregnation, accurate sizing, and an integrated flange.
Compared with conventional externally lubricated bronze bushings, the product can reduce maintenance frequency, contamination risk, lubricant dependence, and downtime. Compared with some plastic alternatives, it offers strong load support and better stability in many elevated-temperature applications. Compared with more complex rolling bearing systems, it provides a compact and simple sliding solution for suitable speed and load ranges.
Reliable results depend on correct selection and installation. Load, speed, PV value, clearance, shaft finish, alignment, temperature, environmental exposure, and housing design must all be considered. With appropriate engineering review, the bushing can provide stable operation, reduced wear, and extended service life.
Jiande Welfine Technology Co., Ltd. supports this product through more than 20 years of powder metallurgy experience, a modern 13,039-square-meter production base, experienced technical personnel, advanced presses and sintering equipment, controlled oil impregnation, precision sizing, OEM and ODM development, and ISO 9001:2015 and IATF 16949:2016 quality systems. These capabilities make it possible to develop customized self-lubricating bushing solutions for demanding industrial and pump applications.
References
1. Powder Metallurgy Materials and Processes, general principles of powder compaction, sintering, sizing, and porosity control.
2. Plain Bearings and Sliding Bearing Engineering, principles of friction, wear, clearance, PV value, and shaft compatibility.
3. Copper and Copper Alloy Engineering Data, general properties and applications of tin bronze materials.
4. Industrial Bearing Selection and Maintenance Practices, guidance on load, speed, temperature, alignment, installation, and service life.
5. ISO 9001:2015, Quality Management Systems—Requirements.
6. IATF 16949:2016, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
7. Powder Metallurgy Component Inspection Practices, principles of density measurement, dimensional control, oil-content verification, and batch traceability.
Product: Powder Metallurgy Self-lubricating Tin Bronze Flanged Bushing
Related products
-
-
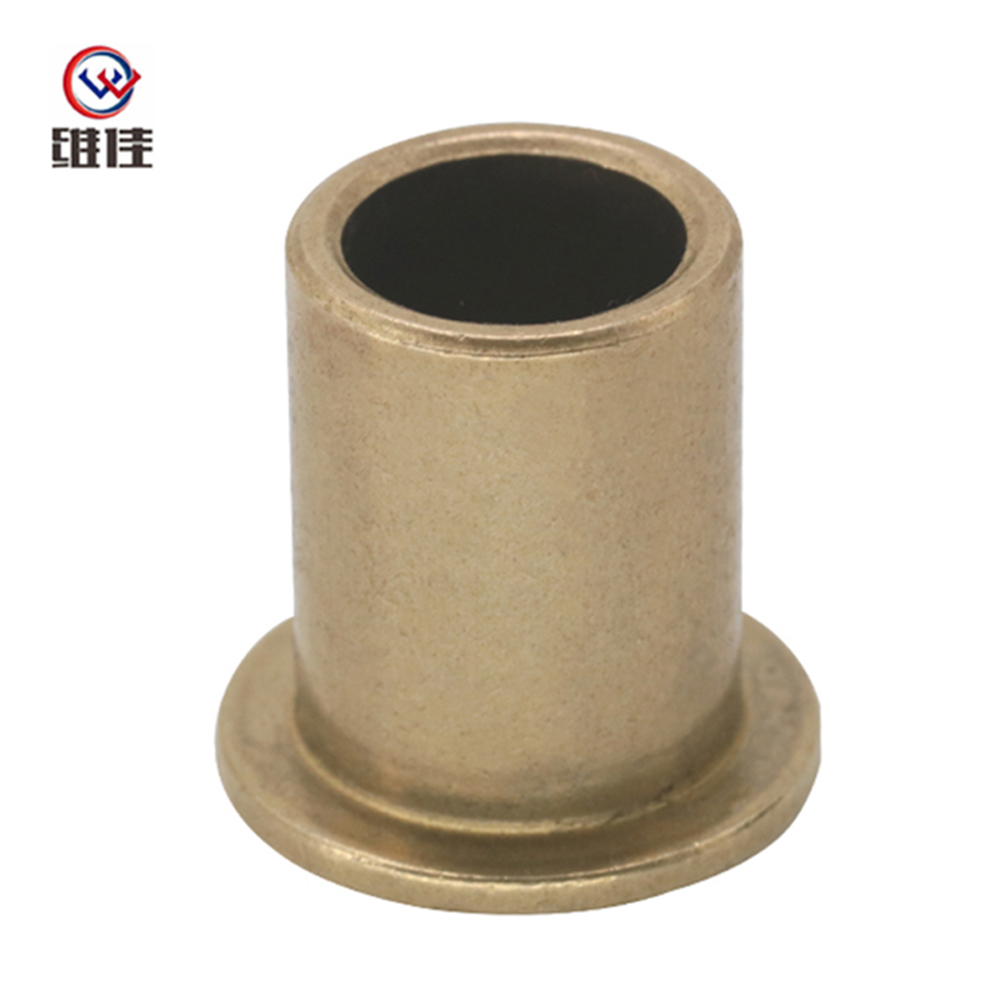
Our sintered bronze self-lubricating bearings are engineered for demanding industrial applications where traditional lubrication is impractical. Designed with advanced powder metallurgy technology, th...
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Privacy Custom Self-lubricating Sintered Bushing Manufacturers
